Como escolher o medidor de vazão de gás adequado para a sua aplicação

Este guia destina-se a pessoas que projetam, especificam, distribuem ou fazem a manutenção de sistemas de medição de gás. Seu objetivo é eliminar as incertezas na escolha de um medidor em ambientes complexos da indústria e do setor de serviços públicos.
1. Por que é importante escolher o medidor de vazão de gás certo em aplicações industriais
Um medidor de vazão de gás raramente apresenta falha logo no primeiro dia. O problema só aparece meses depois. O motor de cogeração de uma usina de biogás começa a oscilar porque o medidor não consegue detectar vazões baixas à noite. Uma auditoria de ar comprimido revela um “déficit” de ar de 12% que ninguém consegue localizar. Um inspetor da concessionária sinaliza um medidor de faturamento que nunca foi aprovado para uso fiscal.
Quase todos esses problemas têm origem na fase de especificação. Ninguém fabricou o medidor de forma inadequada. Ele simplesmente foi escolhido para a aplicação errada.
Uma má seleção custa dinheiro de três maneiras:
- Ineficiência do sistema. Um medidor superdimensionado fica na parte inferior de sua faixa de medição, onde a precisão deixa a desejar. Um medidor com grande queda de pressão faz com que o compressor ou o soprador trabalhem mais intensamente a cada hora, durante anos.
- Risco de conformidade. Um medidor sem a devida aprovação fiscal (baseada em NMI, MID, OIML ou AGA) não pode ser utilizado para faturamento. Um medidor sem certificação ATEX ou IECEx não pode ser instalado legalmente em uma área da Zona 1.
- Custo mais elevado ao longo do ciclo de vida. As intervenções para recalibração, a substituição de rolamentos, as paradas não planejadas e o desperdício de energia costumam representar um custo total de duas ou três vezes o preço de compra.
Cada um dos nossos grupos de clientes enfrenta um desafio específico. Os fabricantes de skids OEM precisam de medidores compactos que se integrem perfeitamente e não gerem chamadas de assistência técnica relacionadas à garantia. As empreiteiras EPC e os integradores de sistemas precisam de medidores que sejam colocados em operação na primeira tentativa e se comuniquem com o sistema de controle. As operadoras municipais precisam de medidores que funcionem por anos em estações não supervisionadas.
A mensagem central deste guia é simples: deixe que a aplicação determine a escolha, e não o preço. O medidor mais barato na cotação costuma ser o mais caro no balanço patrimonial.
2. Compreendendo sua aplicação: a base para a seleção do medidor de vazão
É preciso entender o processo antes de comparar as tecnologias dos medidores. Cinco variáveis são as principais responsáveis por isso.
As cinco variáveis que determinam a escolha do 80%
| Variável | O que perguntar | Por que isso é importante |
|---|---|---|
| Tipo de gás | Gás natural, biogás, ar comprimido, N₂, O₂, H₂, CO₂, gás de queima? | Alguns medidores (térmicos, ultrassônicos) são sensíveis à composição do gás. Outros (Coriolis, de turbina) são muito menos sensíveis. |
| Pressão de operação | Mínimo, normal, máximo (bar g) | A densidade do gás varia com a pressão. O gás a baixa pressão dificulta a medição com medidores de vórtice e de Coriolis. |
| Temperatura | Faixa de temperatura do processo e ambiente | Isso determina as necessidades de compensação, os materiais das vedações e as especificações dos componentes eletrônicos. |
| Faixa de vazão | Mínimo, normal, máximo (Nm³/h ou kg/h) | Isso define o turndown necessário. É a variável mais comumente mal avaliada. |
| Diâmetro do tubo | DN, programação, material, comprimento contínuo disponível | Isso determina se serão utilizados medidores embutidos ou de inserção e define o custo da instalação. |
Definição: Nm³/h (metros cúbicos normais por hora). Trata-se do volume do gás corrigido para uma condição de referência, geralmente 0 °C e 1,01325 bar. Isso permite comparar os fluxos de gás de maneira justa, mesmo quando a pressão na tubulação varia. Um metro cúbico de ar a 7 bar g contém aproximadamente oito vezes mais gás do que um metro cúbico à pressão atmosférica.
Desafios para fabricantes e integradores de skids
As adaptações e ampliações são as que mais causam erros de seleção. Aqui estão três padrões que observamos repetidamente:
- Fluxo projetado x fluxo real. Um skid pode ter sido projetado para 1.000 Nm³/h, mas funcionar na faixa de 250 a 400 Nm³/h durante a maior parte de sua vida útil. Um medidor dimensionado para o vazão de projeto passa, então, toda a sua vida útil na parte inferior da faixa, onde a vazão é mais baixa.
- Especificações para copiar e colar. Um medidor que funcionava em um skid de gás natural a 6 bar é reutilizado em um skid de biogás a 30 mbar. O fenômeno de desprendimento de vórtices pode se tornar instável com essa baixa densidade do gás.
- Ocupação de espaço reduzida. Os conjuntos de tubulação dos fabricantes de equipamento original (OEM) geralmente deixam apenas 3 a 5 diâmetros de tubo (D) retos. Muitos medidores precisam de 15 a 20D para atingir sua precisão nominal.
Estabilidade do processo e meio ambiente
Pergunte se o processo é estável. O fluxo pulsante a jusante de compressores alternativos ou sopradores de lóbulo rotativo pode fazer com que os medidores de turbina apresentem uma leitura superior à real em vários pontos percentuais.
Em seguida, analise o ambiente. O local é classificado como área de risco? O medidor fica ao ar livre a −30 °C ou sob o sol direto do deserto? Ele estará sujeito a condensação, poeira ou vibração? Essas perguntas filtram as opções antes mesmo de se levar em conta a precisão.
Análise do setor: A mistura de hidrogênio nas redes de gás natural está passando da fase piloto para a prática em algumas regiões da Europa, do Reino Unido e da Austrália. As operadoras que hoje especificam medidores para uma vida útil de 15 a 20 anos devem consultar diretamente os fornecedores sobre o desempenho com misturas de hidrogênio. Medidores térmicos e ultrassônicos podem precisar de calibração ou configuração específica para o gás quando a composição da mistura for alterada.
3. Critérios críticos de seleção: precisão, repetibilidade, queda de pressão e relação de turndown
Precisão x repetibilidade
Precisão é o quanto a leitura está próxima do vazão real. Repetibilidade é o grau de consistência com que o medidor apresenta a mesma leitura nas mesmas condições, repetidamente.
Aqui está um exemplo simples. Imagine um jogador de dardos que sempre acerta o mesmo ponto, duas polegadas à esquerda do centro do alvo. Esse jogador tem grande consistência, mas não é preciso. A calibração faz com que o conjunto de dardos atinja o centro do alvo.
Ambos são importantes, mas em aspectos diferentes:
- Transferência de custódia (faturamento entre comprador e vendedor) exige ambos, comprovados por um certificado de calibração rastreável. Um erro de 1% em uma linha que transporta $2 milhões de gás por ano representa $20.000 indo para a parte errada.
- Controle de processos (razão do queimador, mistura, circuitos PID) prioriza acima de tudo a repetibilidade. Um controlador pode funcionar bem com um pequeno desvio fixo. Ele não consegue funcionar com uma leitura que oscila.
Preste atenção às letras miúdas: “±1% da leitura” e “±1% da escala total” são especificações muito diferentes. A 10% de vazão total, um medidor com tolerância de ±1% da escala total pode apresentar um desvio de ±10% em relação à leitura real.
Queda de pressão e projeto de skid com eficiência energética
Perda de pressão permanente é a pressão que o gás nunca recupera depois de passar pelo medidor. Seu compressor ou soprador precisa compensar essa diferença.
Considere uma tubulação de gás natural DN150 operando a 4 bar g com vazão de 5.000 Nm³/h. Uma perda permanente de 150 mbar em uma placa orificiada requer cerca de 6 kW de potência de compressão adicional. Em mais de 8.000 horas de operação a $0,075/kWh, isso equivale a cerca de $3.600 por ano, todos os anos. Medidores ultrassônicos de passagem total e medidores térmicos de inserção praticamente não causam perda permanente.
Relação de redução para cargas variáveis
Relação de redução é a relação entre o vazão máxima precisa e a vazão mínima precisa. Um medidor com relação de 100:1, com capacidade nominal de 1.000 Nm³/h, mantém a precisão até 10 Nm³/h. Um medidor com relação de 4:1 perde precisão abaixo de 250 Nm³/h.
Uma alta relação de regulação é fundamental para usinas de biogás (a produção do digestor varia de acordo com a matéria-prima e a estação do ano), para o controle de queimadores (fogo baixo x fogo alto) e para redes de ar comprimido (cargas decorrentes de vazamentos à noite e nos finais de semana x produção total).
Valores indicativos para modelos industriais padrão. A faixa de regulação real depende do tamanho, da pressão, da densidade do gás e do fabricante.
Orientações para equipes de MRO
As equipes de manutenção e reparo (MRO) devem fazer três perguntas antes de emitir a ordem de compra:
- O equipamento possui peças móveis? Rolamentos e rotores sofrem desgaste. Modelos sem peças móveis (térmicos, de vórtice, ultrassônicos, de Coriolis ou de orifício) geralmente exigem menos intervalos entre as revisões.
- É possível verificar isso sem precisar desmontar? Os sistemas de diagnóstico a bordo ou as verificações do ponto zero evitam a necessidade de desligar o equipamento e de ir ao laboratório de calibração.
- Como se manifesta a deriva? Peça ao fornecedor dados de campo sobre a variação na calibração após 12 e 24 meses, e não apenas a precisão no primeiro dia.
4. Análise comparativa de 10 tecnologias de medidores de vazão de gás
4.1 Pressão diferencial (placa de orifício)

Um placa de orifício é uma placa fina com um orifício preciso, fixada entre flanges. O gás acelera ao passar pelo orifício e cria uma diferença de pressão (DP). Um transmissor de DP mede essa diferença, e um computador de vazão a converte em vazão.
- Prós: Universalmente aceito e padronizado (ISO 5167, Relatório AGA nº 3). Não é necessário nenhum equipamento de calibração, pois o vazão é calculado a partir da geometria. Baixo custo de hardware.
- Contras: Baixa relação de regulação (cerca de 3–4:1 por transmissor). Alta perda de pressão permanente. Requer trechos retos longos. A precisão diminui quando a borda da placa se desgasta ou fica suja.
- Uso ideal: Gás natural de grande diâmetro, cuja norma está prevista nos contratos, e gás de alta temperatura ou alta pressão.
- Compatibilidade OEM: Moderado. É necessário uma placa, um transmissor, linhas de impulso e, muitas vezes, um computador de vazão, o que significa mais peças para integrar.
- Manutenção: Inspecione a placa anualmente para verificar se há desgaste nas bordas, verifique se há obstruções ou vazamentos nas linhas de impulso e verifique o ponto zero do transmissor.
4.2 Medidores de vazão mássica térmicos
A medidor de vazão mássica térmico mede a quantidade de calor que o gás em movimento retira de um sensor aquecido. Quanto mais moléculas de gás passam, maior é o resfriamento. Assim, o medidor indica diretamente o fluxo mássico, sem necessidade de compensação separada de pressão ou temperatura.
- Prós: Ampla faixa de regulação (100:1 é comum). Queda de pressão muito baixa. Excelente sensibilidade a baixos caudais. As versões de inserção são adequadas para tubos de grande diâmetro a um custo baixo.
- Contras: Calibrado para uma mistura específica de gases; portanto, alterações na composição alteram a leitura. Gotas de líquido no sensor causam picos falsos.
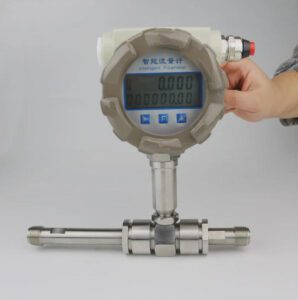
- Uso ideal: Auditorias de ar comprimido, biogás, gás de digestor, gás de queima e ar de combustão de queimadores. Nossas medidor térmico de vazão mássica de gás é frequentemente especificado para essas aplicações.
- Compatibilidade OEM: Excelente. É compacto, um único dispositivo faz tudo e oferece saídas de 4–20 mA, de pulso e Modbus.
- Manutenção: Limpe o sensor periodicamente em caso de gás sujo. Verifique novamente a calibração do gás caso haja alteração no gás de processo.
4.3 Ultrasonic Flow Meters (Transit-Time)

Transit-time meters send sound pulses across the pipe, with the flow and against it. A pulse traveling with the flow arrives slightly sooner. The time difference gives the gas velocity.
- Prós: No moving parts and essentially zero pressure loss in full-bore designs. Wide turndown. Rich diagnostics such as speed of sound, gain, and path-by-path velocity. Multipath meters are the benchmark for large custody transfer.
- Contras: High upfront cost for multipath inline meters. Sensitive to pulsation noise from pressure-reducing valves. Low-pressure gas weakens the acoustic signal.
- Uso ideal: Transmission and distribution custody transfer, large-bore process gas, and bidirectional storage lines. The AGA Report No. 9 overview from ASGMT explains the performance requirements for fiscal use.
- Compatibilidade OEM: Good for larger skids. It has digital outputs and needs a little more commissioning expertise.
- Manutenção: Low. Trend the diagnostics and verify speed of sound against a gas composition calculation.
4.4 Vortex Shedding Flow Meters

A bluff body in the pipe sheds swirling eddies, first on one side and then the other. This is the Kármán vortex street effect. The shedding frequency rises in step with velocity.
- Prós: No moving parts, handles steam and gas, and is robust at high temperatures. Built-in temperature and pressure compensation makes it a practical one-box solution.
- Contras: Needs a minimum velocity, so it goes blind at very low flow. Sensitive to pipe vibration. Needs 15–30D of upstream straight run.
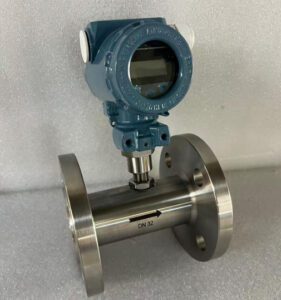
- Uso ideal: Plant utilities, steam, compressed air mains, and nitrogen headers. See our vortex flow meter with integrated T/P compensation.
- Compatibilidade OEM: Good. It comes in standard flanged or wafer sizes.
- Manutenção: Low. Check the sensor for fouling and review vibration if readings get noisy at low flow.
4.5 Turbine Flow Meters
A bladed rotor spins in the gas stream at a speed proportional to velocity.
- Prós: High accuracy on clean, steady gas. Proven for fiscal use under AGA Report No. 7. Fast response and a moderate price.
- Contras: Bearings wear. Over-reads in pulsating flow. Damaged by debris and liquid slugs. Needs upstream filtration.
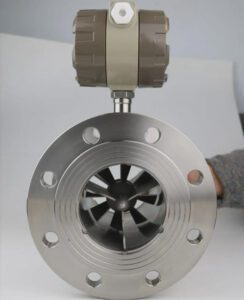
- Uso ideal: Clean natural gas distribution and industrial metering. Our gas and steam turbine flow meter line covers these duties.
- Compatibilidade OEM: Good. It gives a standard pulse output.
- Manutenção: Moderate. Lubricate bearings (on some models), check the rotor, and recalibrate every 1–3 years.
4.6 Coriolis Mass Flow Meters

Gas flows through vibrating tubes. The mass flow creates a tiny twist in the tubes, and sensors measure it. Coriolis is the only common technology that measures mass directly, whatever the gas composition.
- Prós: Very high accuracy (±0.35–0.5% for gas on many models). Unaffected by composition changes. No straight run needed.
- Contras: Expensive. Heavy in larger sizes. Practical size limits (usually DN150 and below for gas). Noticeable pressure drop at low line pressure.
- Uso ideal: CNG and hydrogen dispensers, specialty gas blending, and high-value gas where composition varies.
- Compatibilidade OEM: Excellent for compact dispensing skids.
- Manutenção: Low. Verify zero in the field and use the tube health diagnostics.
4.7 Diaphragm Meters (Low-Flow Utility Use)

Flexible diaphragms fill and empty measuring chambers of known volume. Every cycle counts a fixed amount of gas.
- Prós: Very wide turndown (a G4 meter covers roughly 0.04–6 m³/h, or 150:1). Needs no power. Very low cost per point. Accepted for billing almost everywhere.
- Contras: Low pressure only (usually below 0.5 bar). Bulky for the flow they handle. Not suitable for process control.
- Uso ideal: Residential, small commercial, and light industrial billing.
- Compatibilidade OEM: Limited. Pulse or smart-module add-ons are available.
- Manutenção: Nearly none. Utilities replace or sample-test by population.
4.8 Rotary Meters
Two figure-eight lobes rotate and trap fixed volumes of gas. This is positive displacement at higher pressures and flows than diaphragm meters.
- Prós: High accuracy and wide turndown. No straight-run requirement. Compact for commercial and industrial billing.
- Contras: Can stall and block flow if debris jams the lobes. Needs filtration and correct lubrication. Slight noise and pulsation.
- Uso ideal: Commercial and industrial gas billing from about 16 to 1,000 m³/h.
- Compatibilidade OEM: Moderate. It’s heavy but has a small footprint.
- Manutenção: Change the oil, check differential pressure across the meter (a rising DP warns of wear), and keep the filter clean.
4.9 Variable Area (Rotameter)

A float rises in a tapered tube until the gas flow balances its weight. You read the flow from a scale.
- Prós: Very cheap. Needs no power. Instant visual indication. Metal-tube versions add a 4–20 mA output.
- Contras: Low accuracy (±2–5% of full scale). Must be mounted vertically. Calibrated for one gas at one pressure.
- Uso ideal: Purge gas, analyzer sample lines, and local indication on OEM machines.
- Compatibilidade OEM: Excellent for simple indication.
- Manutenção: Clean the tube and float, and check for sticking.
4.10 Pitot Tube Meters
A pitot tube, or its multi-port averaging version, senses the difference between impact pressure and static pressure across the pipe.
- Prós: Low permanent pressure loss. Hot-tap insertion without shutdown. Cheap in very large ducts.
- Contras: Low turndown. Weak signal at low velocity. Ports plug in dirty gas.
- Uso ideal: Large air ducts, combustion air, and stack flow.
- Compatibilidade OEM: Good for large ductwork.
- Manutenção: Purge ports on dirty service and check transmitter zero.
Side-by-side summary
| Tecnologia | Typical Accuracy (Gas) | Serviço de arrumação | Pressure Loss | Peças móveis | Relative Cost | Best Fit |
|---|---|---|---|---|---|---|
| Placa de orifício | ±0.6–2% of rate | 3–4:1 | Alta | Não | Low (element) | Standardized large-bore NG |
| Thermal mass | ±1–1.5% of reading | 100:1 | Muito baixo | Não | Low–Medium | Compressed air, biogas, flare |
| Ultrasonic (multipath) | ±0.1–0.5% (calibrated) | 50–100:1 | Nenhum | Não | Alta | Custody transfer, large pipes |
| Vórtice | ±1% of reading | 20–30:1 | Médio | Não | Médio | Utilities, steam, air mains |
| Turbina | ±0,5–1% | 10–30:1 | Médio | Sim | Médio | Clean NG distribution |
| Coriolis | ±0.35–0.5% | 20–100:1 | Medium–High | Não | Very high | CNG, H₂, specialty gas |
| Diaphragm | Class 1.5 | 150:1 | Baixa | Sim | Muito baixo | Residential billing |
| Rotary | ±0,5–1% | 30–160:1 | Baixa | Sim | Médio | Commercial billing |
| Rotameter | ±2–5% FS | 10:1 | Baixa | Float | Muito baixo | Purge, local indication |
| Pitot/averaging pitot | ±1–2% | 3–10:1 | Muito baixo | Não | Baixa | Large ducts |
Figures are indicative. Always confirm against the datasheet for the model and size you’re considering.
5. Technology Match: Aligning Meter Types with Industry-Specific Needs
OEM equipment and skid-mount manufacturers
OEMs care about three things: space, integration, and a low warranty-return rate. A compact all-in-one meter with built-in compensation removes a flow computer from the bill of materials. Calibration flexibility also matters. One mechanical design that can be factory-configured for air, N₂, or natural gas simplifies your inventory.
Common match: Thermal mass meters for burner and air skids, vortex meters for utility skids, and Coriolis meters for dispensing.
A burner OEM we work with standardized on one insertion thermal model across three skid sizes. They cut their meter part numbers from nine to three and removed separate P/T transmitters from every skid.
EPC contractors and system integrators
For EPC and integration teams, the hidden cost is commissioning hours. Look for these:
- A native HART protocol over 4–20 mA for asset management systems
- Modbus RTU/TCP register maps delivered with the documentation, based on the open Modbus specification
- DD/DTM files ready before site acceptance testing
- Clear straight-run and orientation drawings for the piping designers
Common match: Vortex meters for plant utilities, ultrasonic meters for large headers, and orifice plates where the client standard demands them.
Municipal utilities
Unmanned stations need meters that survive without supervision. Look for weather-rated enclosures, battery or low-power options, and legal-metrology approval. Examples include NMI (Australia), MID (Europe), or pattern approval based on OIML recommendations such as R 137.
Common match: Diaphragm and rotary meters for billing, ultrasonic meters for district metering, and thermal meters for digester gas at wastewater plants.
Industrial terminals and MRO companies
For terminals and MRO teams, uptime is everything. Ask for spare part lead times, published MTBF figures, and diagnostics that separate “the meter is failing” from “the process changed.”
Definition: MTBF (Mean Time Between Failures). This is the average operating time between failures. An MTBF of 100,000 hours means that, across a large population of meters, failures average about once every 11 years per device.
Common match: No-moving-parts technologies that report their own health.
Instrument importers and distributors
Distributors sell trust along with hardware. Your supplier needs to back you up with multi-region certificates (ATEX, IECEx, and local approvals), English and local-language manuals, application support, and training. The gas flow meter selection guide written for distributors from Jade Ant Instruments covers the needs-assessment questions to ask before quoting.
6. Installation, Calibration, and Environmental Considerations
The most common installation mistakes
- Too little straight run. A meter installed 3D after a double elbow reads a swirled, distorted profile. Errors of 2–5% are common with vortex, turbine, and single-path ultrasonic meters.
- Wrong orientation. Rotameters must be vertical. Some vortex meters need the transmitter head positioned so condensate doesn’t collect at the sensor in wet gas.
- Temperature and pressure compensation gaps. A volumetric meter reading actual m³/h without P/T correction can be 20–30% off the standard-volume figure the accounting team expects.
- Poor grounding and cable routing. VFD noise can put phantom pulses on turbine and vortex signals.
Typical straight-run requirements
| Tecnologia | Upstream | A jusante | Notas |
|---|---|---|---|
| Placa de orifício | 20–40D | 5–8D | Flow conditioner can reduce this |
| Vórtice | 15–30D | 5D | 30D after two elbows in different planes |
| Turbina | 10–20D | 5D | Add filtration upstream |
| Thermal (insertion) | 15–20D | 5D | Profile-sensitive at a single point |
| Ultrasonic (multipath) | 10–20D | 3–5D | Fewer paths need more straight run |
| Coriolis | 0D | 0D | Mount stress-free |
| Rotary / diaphragm | 0D | 0D | Filter upstream |
D = pipe inside diameter. For a DN100 line, 20D is about 2 meters.
Best practices for low noise and long-term accuracy
- Use shielded twisted-pair cable, ground it at one end only, and keep it separate from VFD power cables.
- Install pulsation dampers or move the meter away from reciprocating compressors.
- Put the meter downstream of pressure-reducing valves only if there’s enough distance. Valve noise can swamp ultrasonic signals.
- Record an “as-found” baseline of diagnostics at commissioning so later drift is easy to spot.
Hazardous area certifications
In oil and gas plants, chemical sites, and biogas facilities, the electrical certification matters as much as the accuracy.
- ATEX: The EU framework for equipment in explosive atmospheres. The ATEX directive defines equipment categories that line up with zones.
- IECEx: The international scheme, accepted in many countries outside the EU. You can check certificates on the IECEx certification portal.
- FM / CSA / UL: Required for North American Class/Division areas.
Definition: Zone 1. This is an area where an explosive gas atmosphere is likely during normal operation. Zone 1 meters typically carry an Ex d (flameproof) or Ex ia/ib (intrinsically safe) rating, such as Ex d IIC T6 Gb.
For more detail on acoustic meters in dangerous services, see our article on ultrasonic meters for hazardous fluid monitoring.
7. Lifecycle Cost Analysis: Beyond the Initial Purchase Price
The Total Cost of Ownership (TCO) model
TCO = Purchase + Installation + Calibration + Maintenance + Energy Loss + Downtime + End-of-Life Replacement
For most industrial gas meters, the purchase price is only 25–40% of the 10-year cost.
This is an indicative split for a mid-size mechanical meter in general industrial service. Your mix will vary with duty and location.
Case example: ultrasonic vs. orifice in a natural gas distribution skid
Scenario: A DN150 natural gas distribution skid runs at 4 bar g, carries an average flow of 5,000 Nm³/h, and operates 8,000 hours a year.
| Cost Item (5 Years) | Orifice Plate System | Inline 2-Path Ultrasonic |
|---|---|---|
| Purchase + installation (plate, meter tube, DP transmitter, flow computer vs. meter + electronics) | $9,500 | $22,000 |
| Maintenance (plate inspection, impulse lines, transmitter checks) | $9,000 | $2,000 |
| Energy loss (150 mbar permanent loss, ~48,000 kWh/yr at $0.075) | $18,000 | ~$0 |
| Downtime (2 plate change-outs with bypass operation) | $4,000 | $0 |
| Field verification (diagnostic review) | $0 | $1,500 |
| 5-year total | $40,500 | $25,500 |
The ultrasonic meter costs $12,500 more upfront but saves about $15,000 over five years. That leaves out a bigger lever: measurement uncertainty. This line moves about 40 million Nm³ a year. If better turndown and diagnostics cut the unaccounted-for gas by just 0.2%, that’s another 80,000 Nm³ a year recovered.
ROI justification for continuous processes
A higher-cost meter usually pays back when three conditions are true:
- The process runs more than 6,000 hours a year.
- The gas is valuable, or the meter feeds billing or emissions reporting.
- A shutdown to service the meter is expensive or hard to schedule.
Simple payback = extra upfront cost ÷ annual savings. In the example above, $12,500 ÷ about $3,000 a year gives a payback of roughly 4 years, based on operating savings alone. Many of our EPC clients use a 3-year payback as the approval threshold for continuous-duty plants.
8. Smart Features and Digital Integration for Industry 4.0 Readiness
Digital diagnostics and predictive maintenance
Modern meters can report on their own condition. Examples include signal gain on ultrasonic paths, sensor resistance drift on thermal probes, and shedding signal quality on vortex meters.
Definition: Predictive maintenance. This means servicing equipment based on its measured condition rather than a fixed calendar. Instead of pulling a meter every 12 months “just in case,” you pull it when a diagnostic trend says it’s needed.
A water utility customer that monitors digester gas at three treatment plants moved from annual meter removals to trend-based checks. That cut site visits per meter from four a year to one, and they caught a wet-sensor problem weeks before it would have affected CHP fuel reporting.
IIoT compatibility
Definition: IIoT (Industrial Internet of Things). These are field devices that share data over networks with cloud or edge platforms for analytics.
For system integrators and utility SCADA teams, check for these features:
- Modbus TCP or Ethernet-based protocols on the device, or via a gateway
- Data logging with timestamps, so records survive communication outages
- Wireless options (4G, NB-IoT, LoRaWAN) for remote stations with no cabling budget
- Cybersecurity basics: password-protected configuration and write protection
Preparação para o futuro
Specify meters that allow field firmware updates, multiple output options on one device (4–20 mA plus pulse plus Modbus), and gas-table updates for future blends such as hydrogen in natural gas. A meter that can’t be reconfigured tends to become a stranded asset when the process changes.
Análise do setor: Emissions reporting rules for methane and CO₂ keep tightening in many regions. Flare gas and vent gas meters that once served as rough indicators increasingly need defensible accuracy, audit trails, and traceable calibration. That shift favors meters with self-diagnostics and logged data.
9. 10-Point Evaluation Checklist for Buyers
Use this checklist before any request for quotation (RFQ) goes out. It works for OEMs, EPCs, distributors, MRO teams, and utilities alike.
- Define gas type and composition. Include moisture, H₂S, particulates, and how much the composition varies.
- Confirm operating pressure and temperature range. Give minimum, normal, and maximum values, not just the design values.
- Determine minimum and maximum flow rates. Use logged data where possible, and include night and startup flows.
- Set required accuracy and repeatability. Say whether the meter is for billing, reporting, or control.
- Check pipe size and installation constraints. Note the available straight run, orientation, and access for removal.
- List output signal and communication needs. For example: 4–20 mA, pulse, HART, Modbus RTU/TCP, or wireless.
- List required approvals. For example: ATEX, IECEx, SIL, NMI, MID, OIML, or AGA-based requirements.
- Plan maintenance access and the recalibration interval. Decide on in-situ verification vs. lab calibration.
- Confirm power availability. Loop-powered, 24 VDC, AC, or battery for remote sites.
- Compare lifecycle cost with budget constraints. Put the 5- or 10-year TCO beside the purchase price.
| Checklist Item | Your Value | Notes / Source |
|---|---|---|
| Gas type & composition | ||
| Pressure range (bar g) | ||
| Temperature range (°C) | ||
| Flow range (Nm³/h or kg/h) | ||
| Accuracy / repeatability | ||
| Pipe size & straight run | ||
| Output & protocol | ||
| Approvals | ||
| Maintenance & calibration | ||
| Power | ||
| Budget / TCO target |
Tip: Copy this table into Excel and send it with your RFQ. A complete sheet usually cuts quote turnaround in half and avoids “assumed” values that cause mismatches later.
If you want a second opinion on a completed sheet, the application engineers at Jade Ant Instruments can review it and point out risks before you commit. Send your application data to our engineering team.
Watch: A practical flow meter selection walkthrough
https://www.youtube.com/watch?v=zQOlIZE49O0
This video walks through liquid, gas, steam, and mass flow selection logic. It’s a good primer to share with purchasing or project teams before a technical review.
Glossário de termos-chave
| Termo | Plain-English Meaning | Quick Example |
|---|---|---|
| Transferência de custódia | Measurement that decides a payment between two parties | Gas utility billing a factory |
| Relação de redução | Max accurate flow ÷ min accurate flow | 100:1 means 1,000 down to 10 Nm³/h |
| Repetibilidade | Same reading under the same conditions | ±0.2% repeatability for a burner loop |
| Perda de pressão permanente | Pressure the gas never recovers after the meter | 150 mbar across an orifice |
| Straight run | Clear straight pipe before and after the meter | 20D = 2 m on DN100 |
| Nm³/h | Gas volume at reference conditions | Lets you compare 2 bar and 8 bar flows |
| Compensation | Correcting volume for pressure and temperature | Vortex with built-in P/T sensors |
| Insertion meter | Probe inserted through a fitting into a large pipe | Thermal probe in a DN600 air duct |
| Ex d / Ex ia | Flameproof / intrinsically safe protection types | Zone 1 meter labeled Ex d IIC T6 |
| AGA 3 / 7 / 10 | Orifice / turbine / speed-of-sound standards | AGA 10 checks ultrasonic diagnostics |
10. FAQs: Expert Answers to Real-World Buyer Concerns
1. What is the most accurate gas flow meter for custody transfer applications?
For large pipelines, flow-calibrated multipath ultrasonic meters are the current benchmark, with uncertainty around ±0.1–0.3% after calibration. For smaller, high-value flows with changing composition, Coriolis meters give about ±0.35–0.5% mass accuracy. Turbine and rotary meters are still widely approved for mid-size billing. The “right” answer also depends on which standard your contract or regulator names. Our overview of custody transfer compliance and ROI for natural gas goes deeper.
2. Can thermal mass flow meters measure wet or dirty gases?
With limits. Dust and dry particulates are manageable with periodic sensor cleaning. Liquid droplets are the real problem, because water hitting the heated sensor causes sudden cooling and false high readings. For saturated biogas, use a condensate trap and moisture knockout upstream, plus a sensor designed for wet gas service. Our article on thermal meters in biogas and renewable energy digesters covers practical setups.
3. How does gas composition affect flow measurement accuracy?
It depends on the principle. Thermal meters depend on the gas’s heat properties, so a methane swing from 55% to 65% in biogas can shift the reading by several percent unless the meter is compensated. Ultrasonic meters rely on the speed of sound. Orifice and vortex meters need correct density. Coriolis meters measure mass directly and are least affected. Always give suppliers a realistic composition range, not a single value.
4. What are the advantages of ultrasonic over turbine meters in high-flow applications?
Ultrasonic meters have no moving parts to wear, no pressure loss, wider turndown, and diagnostics that show whether the meter is healthy without removing it. In large pipes (DN200 and above), they also avoid the damage a turbine rotor can suffer from debris or overspeed. Turbines still win on upfront cost in mid sizes and on tolerance to some valve noise.
5. When should I choose Coriolis over thermal for mass flow measurement?
Choose Coriolis when the gas composition varies, when you need the highest accuracy, or when the gas is at high pressure, as with CNG and hydrogen dispensing. Choose thermal when the pipe is large, the pressure is low, the pressure drop must be minimal, or the budget matters. Thermal is also far more practical above DN100. For a deeper look at thermal control options, see thermal mass flow controllers compared with conventional meters.
6. How do I compensate for pressure and temperature variations in my readings?
Either use a meter with built-in P/T compensation (common on vortex and turbine meters) or add pressure and temperature transmitters feeding a flow computer. Mass-based meters like thermal and Coriolis don’t need this step for mass output. For natural gas fiscal work, the flow computer also applies a compressibility calculation such as AGA 8.
7. Are there flow meters that don’t require straight pipe runs?
Yes. Coriolis, rotary, and diaphragm meters need essentially no straight run. Multipath ultrasonic meters and flow conditioners can greatly shorten the requirement for other types. This is often the deciding factor on tight OEM skids.
8. What maintenance is required for vortex shedding meters in industrial settings?
Very little. Inspect the bluff body and sensor for fouling or erosion every 1–3 years, check the process connection gaskets, and review signal quality if low-flow readings get unstable, which usually points to vibration. Our complete vortex meter guide for steam and gas includes a troubleshooting section.
9. Can I integrate a flow meter with my existing PLC/SCADA system?
Almost always. The 4–20 mA and pulse outputs work with any PLC. HART adds diagnostics over the same wires. Modbus RTU/TCP lets you read totals, alarms, and diagnostics directly. Ask the supplier for the register map before purchase so your integrator can prepare the tags ahead of time.
10. How do I verify the calibration of a gas flow meter in the field?
The options include comparing against a reference meter installed in series, using the meter’s built-in verification (zero checks, sensor resistance, speed of sound compared with calculated values), or sending the meter to an accredited lab. For fiscal meters, follow the interval set by your regulator or contract. For process meters, trend the diagnostics and verify when drift appears.
11. What is the typical lifespan of a diaphragm gas meter in municipal applications?
Diaphragm meters typically serve 15–25 years. Many utilities replace or sample-test them by population based on local legal-metrology rules. Service life shortens when the gas is dirty or wet.
12. Are there explosion-proof flow meters suitable for Zone 1 environments?
Yes. Look for ATEX or IECEx marking with equipment protection level Gb or better, such as Ex d IIC T6 Gb or Ex ia IIC T4 Ga. Make sure the gas group (IIA, IIB, IIC) and temperature class match your area classification. Hydrogen needs IIC.
13. How does turndown ratio impact performance in variable-load processes?
If your flow drops below the meter’s minimum, readings become inaccurate or drop to zero. In a burner or digester, that means poor fuel-to-air ratio control and missing gas totals. Size the meter so normal operation sits at 30–70% of its range, and check that the lowest real flow stays above the meter’s minimum.
14. What are the key differences between AGA 3, AGA 7, and AGA 10 standards?
AGA Report No. 3 covers orifice meters: plate design, meter tubes, and flow calculation. AGA Report No. 7 covers turbine meters for natural gas. AGA Report No. 10 isn’t a meter standard at all. It calculates the speed of sound in natural gas from its composition, and it’s widely used to cross-check ultrasonic meter diagnostics. AGA 9 is the ultrasonic meter standard.
15. Can a single flow meter handle both high and low flow rates in biogas recovery systems?
Often yes, if you choose a high-turndown technology. Thermal mass meters with 100:1 or wider turndown are the common choice for digester and landfill gas. When the range is extreme, for example during startup and flaring, some plants install two meters in parallel with automatic switchover. For more selection logic, read our breakdown of 2026 thermal air meter types.
Final Takeaway
Choosing the right gas meter doesn’t mean finding the “best” technology. It means matching a measurement principle to a real process: its gas, its pressure, its flow swings, its installation limits, and its compliance rules. Start with the checklist, run the TCO numbers, and involve your supplier’s engineers early.
For more technical articles, browse the Jade Ant Instruments flow measurement blog. Or start at the Jade Ant Instruments flow meter manufacturer homepage to see the full gas and steam measurement range.