Turbine Flow Meter Guide: Accuracy, Installation and ROI
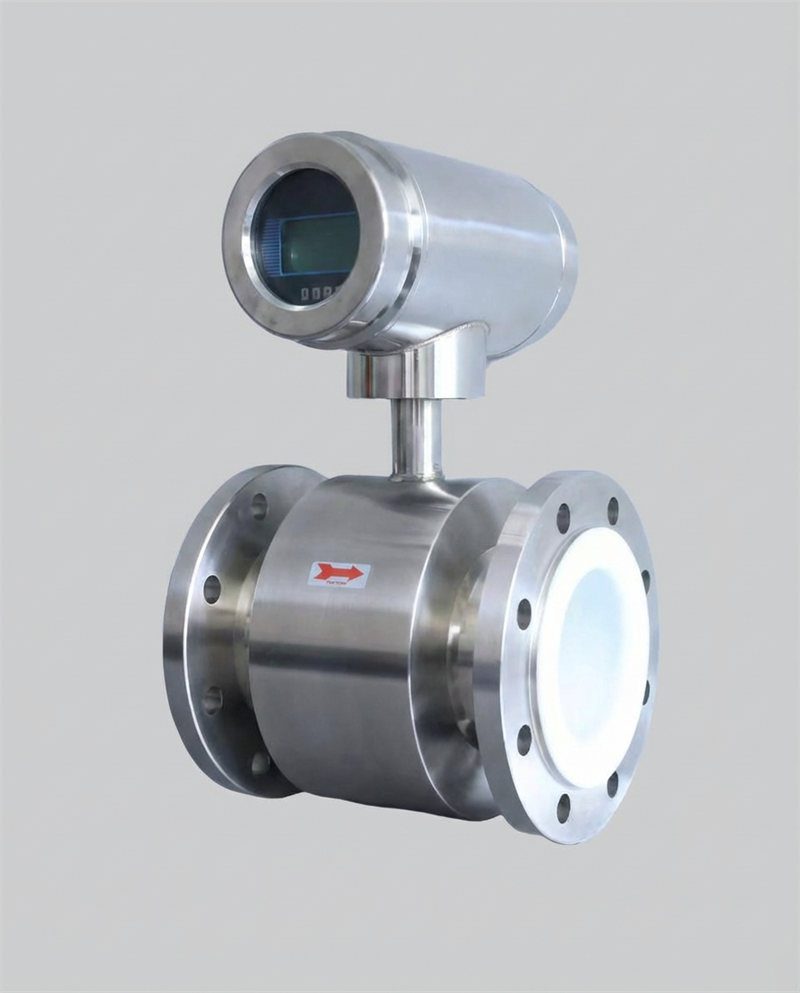
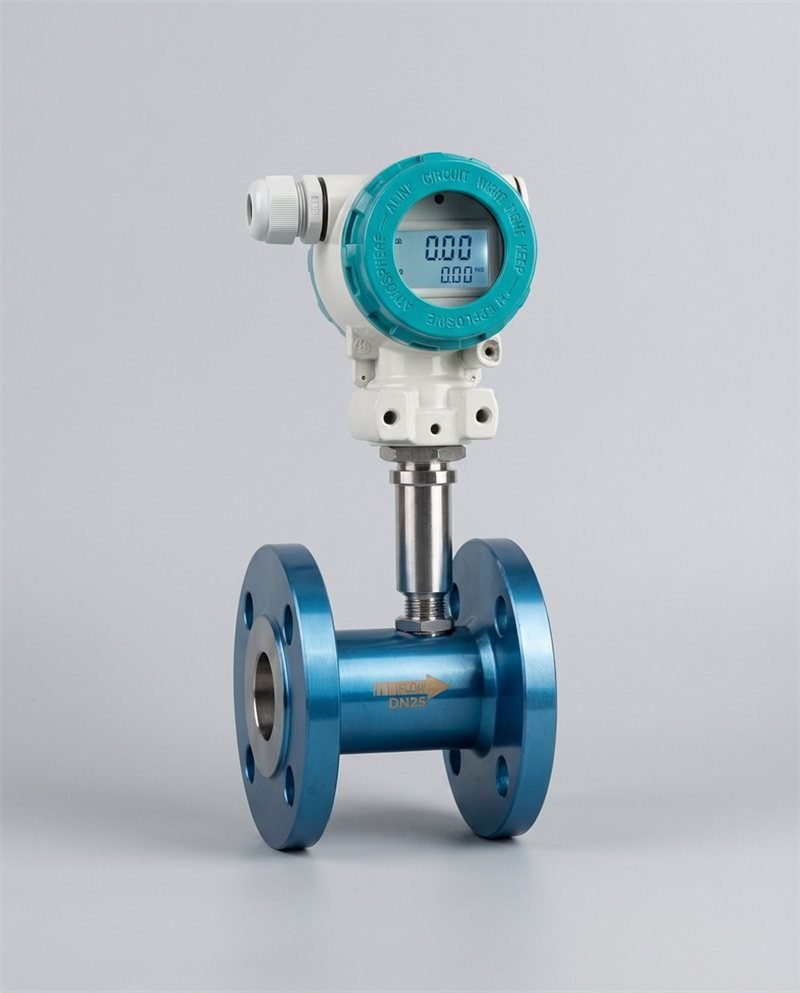
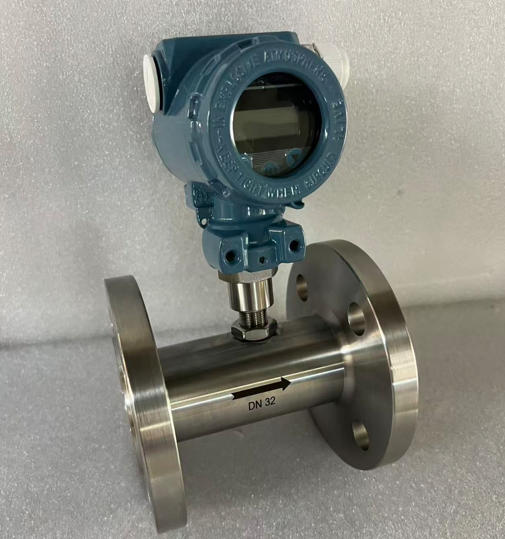
Image: Jade Ant Instruments product photo.
Quick answer: A turbine flow meter measures how fast a small rotor spins in the fluid. It is one of the most accurate and fastest-responding meters for clean, thin liquids and for gas, and it costs less than most alternatives on small pipe sizes. It does need straight pipe, a strainer, and a calibration plan. Get those three right and it works for years. Skip them and it drifts.
I. The Strategic Role of Turbine Flow Meters in Industrial Infrastructure
The critical need for precision in high-stakes fluid management
Every buyer on your side of the table has paid for a bad reading once. An OEM ships a dosing skid and gets a call about batch variance. An EPC hands over a plant and finds the totals do not match the tank gauges. A utility finds that billed water is lower than pumped water.
A small error adds up fast. Jade Ant Instruments’ distributor guide gives a simple case: a 0.5% shift in a turbine meter’s K-factor on a line moving 10 million USD of product a year equals 50,000 USD of fluid nobody can account for.
High-level definition: why the turbine meter is the “precision instrument” of the flow world
A turbine flow meter puts a bladed rotor in the pipe. Moving fluid spins the rotor. A sensor outside the pipe counts each blade as it passes. More spin means more flow.
It earns the “precision instrument” label for three reasons:
- Accuracy. Jade Ant’s guidance puts clean-liquid turbine meters at ±0.25% to ±0.5% of reading, with premium models reaching ±0.1%.
- Speed. The rotor follows flow changes in milliseconds, which matters for batching and fast valve cut-off.
- Size. A DN50 turbine body is only a few pipe diameters long, so it fits on tight skids.
The core value proposition: cost-efficiency with rigorous measurement
Turbine meters are not the right answer everywhere. They are the right answer for clean, low-viscosity liquids and gases where you want high accuracy and a pulse signal at a fair price. This guide shows you where that line sits, so you can say yes with confidence and no without regret. It also covers the installation habits that keep the meter inside its calibration.
Instrumentos Jade Ant builds turbine, magnetic, vortex and ultrasonic meters, so the comparisons below include the cases where we would steer you away from a turbine.
II. Engineering Fundamentals: How Turbine Flow Meters Solve the Measurement Problem
The physics of kinetic energy transfer: from fluid velocity to rotational frequency
Fluid in motion carries kinetic energy, which is the energy of movement. When it hits the angled blades, some of that energy turns the rotor. Faster fluid pushes harder and the rotor spins faster.
Because the pipe has a fixed cross-section, fluid velocity is directly tied to volume flow:

Image: Ruben Castelnuovo, CC BY-SA, via Wikimedia Commons.
The role of the pickup coil and pulse output in digital integration
A pickup coil is a small sensor mounted on the outside of the meter body. Each time a rotor blade passes, the coil sends one electrical pulse. A Hall-effect sensor does the same job using a different method.
Here is why that helps with integration. Pulses are digital. A PLC counter can use them directly, with no signal conversion. The meter’s calibration number, called the Fator K, tells the system how many pulses equal one unit of volume. Turbines Incorporated’s K-factor primer explains how it is found and why it must be re-checked.
Here f is pulse frequency, N is pulse count and K is the K-factor. Here is a worked example with an assumed K of 100 pulses per litre on a DN50 line at 20 m³/h:
- 20 m³/h is 20,000 L per hour, which is 5.56 L per second.
- Frequency = 5.56 × 100 = 556 Hz.
- 10,000 pulses = 100 L of fluid.
Check this early: if your PLC counter tops out at 500 Hz, this meter will under-count at full flow. Jade Ant’s guidance gives the same warning for pulse inputs.
Why linearity matters: consistent accuracy across varying flow rates
Linearity means the K-factor stays the same as flow goes up and down. A perfectly linear meter gives one K for every flow rate. A real meter sags a little at low flow because bearing friction matters more when the rotor is barely turning.
That is why a good calibration certificate lists several points, not one. For tight batching or custody work, ask for the full calibration curve and not only the nominal K. Jade Ant’s accuracy figures also assume a turndown of 10:1 to 20:1. Turndown is the ratio between the highest and lowest flow the meter reads within spec.
Industry insight: Most turbine accuracy complaints start at the low end. A meter sized for peak flow that runs at 5% of range most of the day spends most of its life outside its accuracy window. Size it for the flow you see every day, then check that the peak is still inside the range.
III. Application Mapping: Where Turbine Meters Outperform Other Technologies
| Aplicativo | Why turbine fits | Watch out for |
|---|---|---|
| High pressure / high temperature lines (EPC) | Simple mechanical sensor; pressure ratings up to 420 bar on custody designs; –40 to +200 °C standard | Seal and bearing material at the hot end |
| Fuel and chemical dosing (OEM skids) | Millisecond response, direct pulse to batch controller | Viscosity swings between cold start and warm running |
| Treated water distribution (municipal) | Low cost on DN15–DN300, proven for billing | Grit or raw water destroys bearings |
High-pressure and high-temperature environments for EPCs and system integrators
Jade Ant’s selection table lists –40 to +200 °C for standard liquid turbine meters, up to +250 °C on high-temperature designs, and pressure up to 420 bar for custody-transfer builds. Above 250 °C, the same table points you to vortex meters.
Gas lines have their own model. Jade Ant’s gas and steam turbine flowmeter is specified for DN15–DN300, –20 to +300 °C, up to 10 MPa, with 0.5% standard accuracy and 0.2% as a high-precision option. Outputs are 4–20 mA, pulse and RS485 Modbus.
Steam is a point of care. The distributor guide sends most steam work to vortex meters, while the product page lists steam as a rated medium for the gas and steam model. Check the exact model and operating condition before you commit.
If a hazardous area is involved, look up the certificate yourself. The IECEx system lists approved certification bodies, and certification belongs to a specific model, not a product family.
Precise chemical and fuel dosing for OEM skid-mount manufacturers
Dosing is where the turbine’s speed pays off. A batch controller closes a valve when the pulse count reaches the target. The faster the meter responds, the less overfill you get.
Here is a worked example with assumed numbers. A fuel blending skid doses 500 L per batch. A meter with ±0.5% accuracy can be off by 2.5 L per batch. At ±0.25%, that falls to 1.25 L. At 40 batches a day, the gap is 50 L a day of product you either give away or short your customer.
Jade Ant’s guidance fits this application well: ethanol, acetone, methanol, de-ionized water, diesel and light solvents are all in the sweet spot. Sanitary versions with tri-clamp ends exist for food and pharma.
Large-scale water and utility distribution for municipal infrastructure
In filtered, treated water, turbine meters often cost less than electromagnetic alternatives and meet billing accuracy. The Jade Ant distributor guide cites ±1.0% for treated distribution meters from DN13 to DN300.
The hard rule is “treated only.” Raw water with sand and grit wears bearings within months. For raw water, pump stations and wastewater, choose a magnetic meter instead.
Image: Jade Ant Instruments product photo. A battery-powered unit with a local display suits remote pump stations with no mains supply.
IV. The “Trust Factor”: Why Procurement Professionals Specify Turbine Meters
Proven track record of repeatability and long-term stability
Repetibilidade is how closely a meter repeats itself under the same conditions. It is often better than absolute accuracy, and it is the number batch plants care about most. Jade Ant’s chemical-plant guide reports turbine repeatability of about 0.1% on clean service. A specialty chemical plant in that guide held its K-factor within 0.15% over 18 months on methanol feed lines across more than 12,000 batches a year.
Stability depends on cleanliness. The same guide shows a diesel line in Rotterdam where a missed filtration spec caused a 0.3% K-factor shift after 14 months, and a 40-meter bearing replacement that cost 18,000 USD in one unplanned event.
Ease of integration into existing PLC/SCADA systems for MRO companies
Your maintenance team already knows pulses and 4–20 mA. That is a quiet advantage.
| Output | What it carries | Typical use |
|---|---|---|
| Pulse / frequency | Raw rotor signal | Batching and totalizing straight into a PLC counter |
| 4–20 mA | Flow rate as a current | DCS analog input cards of any age |
| HART | Digital data over the same 4–20 mA wires | Remote setup and diagnostics |
| RS485 Modbus RTU | Many values on one cable | SCADA and multi-meter skids |
A smart transmitter needs power, typically 10–30 VDC. A basic passive pickup generates its own small signal and needs none. The Modbus Organization hosts the open specification if your team wants to check register details.
Compliance with international measurement standards
Standards give auditors something to point at. The API Manual of Petroleum Measurement Standards covers turbine meter use in refined product metering. Jade Ant’s distributor guide also lists AGA Report No. 7 and ISO 9951 for gas turbine meters, and FDA 21 CFR Part 211 alignment for pharmaceutical use.
Ask the supplier for this pack before you award the order:
- Calibration certificate with a traceability statement
- ISO 9001 certificate
- CE declaration
- ATEX or IECEx certificate, if the area is classified
- Wetted-material certificates
- Output wiring diagram and register map
V. Addressing the Pain Points: Common Misconceptions vs. Technical Reality
| What buyers hear | What is actually true |
|---|---|
| “Turbine meters are too fragile for industrial use.” | The weak point is dirt, not the design. Hardened bearings and a correct strainer make them last. |
| “They only work for clean water.” | They work on many clean fluids: fuels, solvents, DI water, gases. They fail on slurries and thick oils. |
| “The pressure drop is too high.” | It is higher than a full-bore magnetic meter, but you can calculate it and plan for it. |
Misconception: “Turbine meters are too fragile for industrial use”
Rotor bearings are the wear part, and that is the honest answer. Jade Ant lists tungsten carbide bearings for liquid service and ceramic bearings for longer life in marginal cleanliness. A 25–75 micron strainer upstream is the single biggest factor in bearing life.
A bearing kit runs about 150–400 USD, and a new rotor assembly 200–600 USD. Many designs let you withdraw the internal cartridge and leave the body in the pipe. So “fragile” really means “needs a strainer and a plan.”
Misconception: “They only work for clean water”
The better statement is that they need a clean, low-viscosity, single-phase fluid. That includes far more than water.
| Fluid property | Limit from Jade Ant’s guidance |
|---|---|
| Viscosity | Under 50 cSt preferred; about 100 cSt maximum |
| Solids | None. Filter to 25–75 microns |
| Velocity | 0.3 m/s absolute minimum; 0.5–3 m/s best; 6–10 m/s maximum |
Material choices widen the fluid list. Jade Ant lists 316L stainless as the default, Hastelloy C-276 for dilute acids and chlorinated solvents, titanium for seawater and oxidizing acids, and PEEK rotors where metal contamination is not allowed. Match each material to the fluid at its highest operating temperature, not at room temperature.
The reality of pressure drop: how to calculate and mitigate energy loss
Pressure drop is the pressure the fluid loses passing through the meter. Your pump has to make it up, every hour it runs.
Chart uses midpoints of the DN50 ranges in Jade Ant’s turbine vs ultrasonic comparison: turbine 0.20–0.50 bar, inline ultrasonic 0.01–0.05 bar, clamp-on 0.
Here is the energy math for a DN50 line at 20 m³/h (0.00556 m³/s), with 70% pump-and-motor efficiency, 8,760 hours a year and power at 0.10 USD per kWh.
That is about 2,435 kWh a year, or roughly 244 USD per year for the turbine’s 0.35 bar. At 0.03 bar, the same math gives about 21 USD. The gap is about 223 USD per year, or 2,230 USD over ten years, on one measurement point.
Pressure drop grows with the square of flow, which gives you a useful lever:
If the normal flow is 30% below the rating point, the drop is only about half. At 14 m³/h, a 0.35 bar meter loses about 0.17 bar. Compare that with an orifice plate, whose permanent pressure loss is often higher still.
To cut energy loss without wrecking accuracy:
- Size the meter so the normal flow sits in the upper half of its range.
- Keep the strainer clean, because a clogged basket adds far more drop than the meter does.
- Use a short, full-port strainer rather than a fine one that clogs quickly.
- On large, high-flow lines, consider an ultrasonic or magnetic meter where the pump cost outweighs the turbine’s price advantage.
VI. Selection Criteria for Distributors and Importers: Avoiding Costly Procurement Errors
Matching fluid viscosity to rotor design to prevent measurement drift
Viscosity is how thick a fluid is, and it changes with temperature. Thicker fluid drags on the rotor, so the rotor slows down and the meter reads low. The unit is the centistoke (cSt). Water at 20 °C is about 1 cSt. Motor oil sits at 100–300 cSt.
| Viscosity at the coldest running temperature | What to do |
|---|---|
| Under 10 cSt | Standard turbine meter; best accuracy |
| 10–50 cSt | Calibrate at operating viscosity; confirm range with supplier |
| 50–100 cSt | Edge of the range; ask for a viscosity-matched calibration |
| Over 100 cSt | Use a Coriolis or positive-displacement meter instead |
Industry insight: The mistake we see most is checking viscosity at the warm running temperature only. A glycol or oil that is thin at 60 °C may be four times thicker during a cold start. That is exactly when a batch gets started and the meter reads low.
Material compatibility: stainless steel vs. exotic alloys for aggressive media
Stainless steel is the default. It is not the answer for everything.
| Fluid | Typical material choice |
|---|---|
| Water, fuels, light solvents | Aço inoxidável 316L |
| Dilute acids, chlorinated solvents | Hastelloy C-276 |
| Seawater, strong oxidizing acids | Titânio |
| Pharma, semiconductor (no metal pickup) | PEEK rotor |
Magnetic meters have a similar material map for liners and electrodes. Jade Ant’s liner and electrode selection guide is a good cross-check if your customer is also considering that technology.
Choosing the right connection standards for global interoperability
Wrong flange standard, wrong week. Ask for these on every quote:
| Connection | Where you find it |
|---|---|
| ASME/ANSI flange (150, 300, 600 class) | North America, many oil and gas projects |
| EN/DIN flange (PN16, PN40) | Europe, Middle East, much of Asia |
| NPT or BSP threaded | Small sizes, OEM skids |
| Tri-clamp | Food, beverage, pharma |
Stock fewer variants. Jade Ant’s own guidance for magnetic meters notes that three or four standard configurations cover most distributor orders, and the same logic works for turbine meters. Their turbine flow meter guide for distributors goes through the full selection table and a TCO view. For a wider technology map, the flow meter selection guide walks through the same questions in order.
Image: Jade Ant Instruments technical article illustration.
VII. Installation Excellence: Eliminating the “Installation Error” Gap
The necessity of straight-run piping: solving the turbulence problem
Straight run is the length of straight pipe before and after the meter. Elbows, valves and pumps make the flow swirl. A swirling flow spins the rotor unevenly, and the reading changes.
Jade Ant’s installation numbers are 10–20D upstream and 5D downstream, where D is the pipe’s inner diameter. After a 90° elbow, 20D. After a control valve, 30D. A flow conditioner can bring 20D down to roughly 10D.
On DN50, D is 50 mm. So 30D is 1.5 m of straight pipe behind a control valve. On a compact skid, that is a real constraint, so draw it on the P&ID before the frame is cut.
A flow conditioner is a perforated plate or tube bundle that breaks up swirl. Jade Ant puts the cost at roughly 500–2,000 USD depending on size. For layout detail, see its Guia de práticas recomendadas para instalação de medidores de vazão.
Proper orientation and air-pocket elimination
Air is the other classic cause of “hunting,” which means readings that wander up and down. Jade Ant lists these orientation rules:
- Horizontal with the shaft horizontal is the standard.
- Vertical upward flow is fine, and helps push bubbles through.
- Vertical downward flow is not recommended, because the pipe may not run full and gravity loads the bearing unevenly.
Even a small gasket lip into the bore can disturb the flow at the rotor. Also check the following before startup:
- Gasket bore matches the pipe bore.
- Strainer is installed and clean.
- Line is vented and full.
- Signal cable is shielded twisted pair, grounded at the receiving end only.
- Vibration over about 0.5 g is isolated from the meter body.
- No pulses appear at zero flow. False pulses at zero usually mean electrical noise or vibration.
Calibration requirements: factory vs. field verification for audit trails
A factory calibration sets the K-factor. A field check proves it still holds. Auditors want both.
| Factory calibration | Field verification | |
|---|---|---|
| Purpose | Sets K-factor and curve | Confirms the meter is still in tolerance |
| Method | Lab rig or prover | Master meter, compact prover, tank drawdown, or weigh test |
| Meter removed? | Yes, usually | Often no |
| Output | Certificate and curve | Verification report |
NIST describes how turbine meters are calibrated against a piston prover, which fixes flow from a known displaced volume over measured time. The calibration lab should also state its uncertainty and follow a recognized quality standard such as ISO/IEC 17025. Jade Ant’s turbine-type flow meter installation and calibration guide lays out a seven-step in-situ routine.
Do not change the K-factor in the field until you have ruled out wiring, air, piping and PLC scaling. A changed K can hide a real fault.
VIII. Maintenance Strategies for MRO and Utility Companies: Extending Lifecycle
Predictive maintenance: identifying wear in bearings before failure occurs
Predictive maintenance means fixing something when the data says it is starting to fail, not on a fixed date. Bearing wear is the main long-term threat. Worn bearings add friction, the rotor slows, and the meter under-registers.
Watch for these early signs:
- A slow drift versus an independent reference
- A new rattling or grinding sound at the meter
- A K-factor that moved at the last calibration
- Noisier pulses at moderate flow
The cost of waiting is clear. Jade Ant’s guide shows how a 0.3% K-factor drift on a terminal handling 30 million USD of product a year equals 90,000 USD of unaccounted volume. Compare that with a 150–400 USD bearing kit.
Industry insight: Keep a K-factor history for every meter, tied to its serial number. Three years of small shifts tell a story. Either the fluid is dirtier than planned, the meter is oversized, or the strainer is being ignored.
Cleaning protocols for preventing debris-induced rotor blockage
Debris is the usual cause of “no signal” or “low signal.” A tidy routine looks like this:
- Check strainer differential pressure at startup, then monthly to quarterly.
- Isolate, depressurize, and drain the line before opening anything.
- Inspect the rotor for chips, pitting and deposits under good light.
- Rotate the rotor by hand or with clean air. Never use metal tools on blades.
- Replace damaged blades or the whole rotor assembly.
- Re-verify the K-factor after any repair.
Jade Ant’s gas and steam turbine page also gives a ready-made routine:
| Interval | Tasks |
|---|---|
| Daily / weekly | Watch for odd readings, noise, vibration and visible leaks |
| Monthly | Clean the upstream strainer; check cable connections and conduit seals |
| Quarterly | Archive flow data for trends; inspect gaskets; test 4–20 mA and pulse outputs |
| Annually | Full functional check; consider recalibration; inspect rotor and bearings if accessible |
When to recalibrate: establishing a schedule based on drift tolerance
Start from the application, then tighten or relax using your own data.
| Aplicativo | Typical interval (Jade Ant guidance) |
|---|---|
| Petroleum custody transfer | 6-12 meses |
| Municipal water billing | 12 months (some large revenue meters at 6 months) |
| Pharmaceutical clean utilities | About 12 months |
| General process control | Up to 24–36 months in stable, clean service |
Then use a simple rule once you have two calibration results:
If your limit is 0.25% and the meter drifted 0.05% per month between the last two calibrations, the interval is 5 months. Local regulation always overrides your own calculation. Jade Ant’s magnetic flow meter calibration tips apply the same tiered logic to a different technology, and the traceability and 4:1 reference rules carry over.
IX. Comparative Analysis: Turbine vs. Electromagnetic and Ultrasonic Meters
When to choose turbine over magnetic meters (non-conductive fluids)
A magnetic meter needs a conductive liquid. The rule of thumb is at least about 5 µS/cm, as covered in this magnetic flow meter overview. Fuels, light oils, many solvents, and de-ionized water fall below that, so a magnetic meter cannot read them. A turbine meter does not care about conductivity.
On the flip side, magnetic meters win on dirty, abrasive and conductive fluids, with no moving parts at all. Jade Ant’s guidance sends raw water, wastewater and slurries to electromagnetic meters.
When to choose turbine over ultrasonic (budget vs. precision)
Ultrasonic meters add almost no pressure drop, and clamp-on units need no pipe cutting. The ultrasonic flow meter article explains the transit-time and Doppler methods. They cost more than a small turbine and give less accuracy, especially clamp-on, where Jade Ant’s guide shows 1–3% depending on pipe condition.
Jade Ant’s price ranges for a 4-inch (DN100) line:
| Meter | Typical purchase price |
|---|---|
| Turbina | 1,500–3,500 USD |
| Inline ultrasonic | 3,000–8,000 USD |
| Clamp-on ultrasonic | 4,000–12,000 USD |
So turbine wins on price and accuracy per dollar for small bores in clean liquid. Ultrasonic wins on pressure drop, corrosive fluids, and retrofits with no shutdown window. The full cross-technology picture is in Jade Ant’s ultrasonic, magnetic and turbine comparison, and its Coriolis, magnetic, turbine and ultrasonic guide adds the mass-flow view. If steam is involved, the vortex versus turbine working principle guide shows when vortex takes over.
What it really costs over ten years
Here is Jade Ant’s own 10-year model for a DN50 clean-liquid line. It is honest about where a turbine does not win on cost.
Ranges from Jade Ant’s distributor guide. They assume a fluid throughput of 200,000 USD a year.
The turbine’s range is wide because maintenance depends on how clean the fluid is. Here is where a turbine’s money goes, using the midpoint of each line item in the same model:
The line-item midpoints add up to 14,000 USD, which sits inside Jade Ant’s published 12,000–22,000 USD range. Purchase price is only about 14% of the total. Measurement error and downtime make up more than half. So a turbine meter is only a bargain if the strainer is maintained and the K-factor is checked on schedule.
The “sweet spot”: where turbine meters dominate
A turbine meter is the technically correct choice when most of these are true:
- The fluid is clean, single-phase and under about 50 cSt.
- The fluid is non-conductive or you need a fast pulse for batching.
- The pipe is DN15–DN150 and the budget is tight.
- Normal velocity falls between 0.5 and 3 m/s.
- You have room for straight pipe, or a conditioner.
- You will filter and calibrate on schedule.
Here is a velocity check on DN50, with an area of 0.001963 m²:
So the preferred window on DN50 is 3.5 to 21.2 m³/h. A line running 20 m³/h sits near the top of it. A line running 2 m³/h is below it and needs a smaller meter.
X. Future-Proofing Your Flow Measurement Strategy
Summary of the turbine meter’s role in operational efficiency
Turbine meters earn their place in clean liquid and gas service. They are fast, accurate, compact, and easy to wire into a PLC. They lose when the fluid is dirty, thick, or needs zero pressure drop.
The long-term financial impact of reducing measurement uncertainty
The numbers in this guide point the same way. A 0.5% shift costs 50,000 USD on a 10 million USD line. A missed strainer cost one terminal 18,000 USD in a single event. A 150–400 USD bearing kit costs far less than either. Reduce uncertainty at the source and the savings repeat every year.
Final recommendations by buyer type
| Buyer | What to do first |
|---|---|
| OEM / skid builder | Check cold-start viscosity and pulse-input limits before choosing the model |
| EPC / integrator | Draw straight-run and strainer positions on the P&ID; request certificates before award |
| Instrument distributor | Stock a few core connection standards and sell calibration as a service |
| MRO / terminal | Start a K-factor log per serial number and a strainer check routine |
| Municipal / utility | Confirm treated water only, and check local rules for recalibration intervals |
Call to action: align specifications with operational goals
Send Jade Ant Instruments your fluid, viscosity range, line size, flow range, and site conditions through the Jade Ant contact page. Their application engineers can check straight run, material and output against your drawing before you order.
To see a turbine meter explained step by step, watch this video before your next design review.
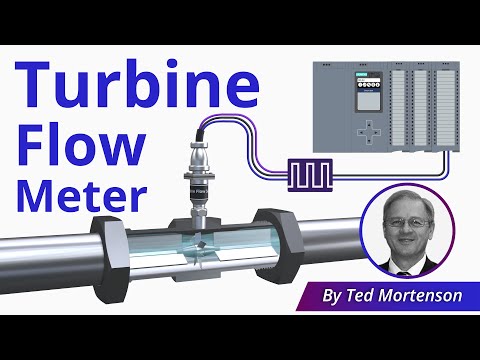
Video: “Turbine Flow Meter Explained | Operation and Calibration.” Click the image to watch on YouTube.
Glossário de termos-chave
Bearing: The part that lets the rotor spin with low friction. It is the main wear part in a turbine meter. Example: a worn bearing makes the meter read low.
Centistoke (cSt): A unit of fluid thickness. Water is about 1 cSt, and turbine meters work best below about 50 cSt.
Flow conditioner: A plate or tube bundle placed upstream that evens out the flow, so you need less straight pipe.
Hall-effect sensor / pickup coil: Two ways to detect rotor blades as they pass. Each blade makes one pulse.
K-factor: The number of pulses the meter makes per unit of volume. Example: K = 100 pulses/L means 10,000 pulses equal 100 L.
Linearity: How constant the K-factor stays across the flow range.
Pressure drop: Pressure lost as fluid passes through the meter. The pump has to make it up.
Repeatability: How closely a meter gives the same reading under the same conditions.
Straight run: The length of straight pipe before and after the meter, measured in pipe diameters (D).
Strainer: A filter basket in front of the meter that catches debris before it reaches the rotor.
Turndown: The ratio between the highest and lowest flow the meter reads within spec. Example: 10:1 on a 21 m³/h meter means it reads down to about 2.1 m³/h.
Perguntas frequentes
1. How does fluid viscosity specifically affect the K-factor of a turbine meter?
Thicker fluid drags on the rotor, so the rotor spins slower than the true fluid speed and the meter reads low. The K-factor therefore changes with viscosity, mostly at lower flow rates. Jade Ant’s guidance suggests staying under 50 cSt where possible, with about 100 cSt as a hard ceiling. Calibrate the meter at the viscosity you will run, and check the cold-start viscosity, since a fluid that is thin when warm can be much thicker at startup.
2. What is the maximum allowable pressure drop for a standard turbine installation?
There is no single legal limit. The right answer is whatever your pump can spare. Jade Ant’s DN50 range is 0.20–0.50 bar, and 0.30–0.70 bar on DN100. Drop rises with the square of flow, so a meter running at 70% of its rating loses only about half as much as at full rating. Use the pump-power formula in Section V to turn bar into watts and dollars, and add the strainer’s drop to the total.
3. Can turbine flow meters handle intermittent air bubbles, and what happens if fluid density changes?
Air is a problem. Jade Ant’s guides note that entrained gas makes a turbine meter read high, and there may be no alarm. Fix it at the source with venting, a deaerator, or a meter location with enough back pressure. For density, a turbine meter measures volume, so a density change affects the mass you calculate, not the volume reading. Use a density input or a Coriolis meter if mass matters. Very light fluids can also reduce the torque on the rotor at low flow.
4. What are the best practices for installing these meters in compact skid-mount designs with limited straight run?
First, put the meter on the longest straight section of the skid. Second, use a flow conditioner to cut the upstream requirement from about 20D to about 10D. Third, keep control valves downstream of the meter, not upstream. Fourth, reduce swirl by avoiding two elbows in different planes right before the meter. If none of that fits, consider a meter with a shorter requirement, such as a magnetic meter at about 5D, or compare it using the flow meter selection guide logic.
5. How do I determine if my fluid is too corrosive for 316L stainless steel rotors?
Start with the fluid, concentration, and the hottest operating temperature. 316L suits water, fuels and light solvents. It can pit in chlorides and many acids. Jade Ant lists Hastelloy C-276 for dilute acids and chlorinated solvents, titanium for seawater and oxidizing acids, and PEEK rotors for metal-free service. Ask the supplier for a compatibility check against your exact fluid list, including cleaning chemicals.
6. What is the typical lifespan of the bearings, and what filtration protects the rotor?
It depends on cleanliness more than on hours. Jade Ant’s chemical-plant guide shows 12–24 months between bearing checks on a continuous line, and as short as 6 months on low-lubricity solvents like acetone. For protection, Jade Ant specifies a 25–75 micron strainer upstream of every turbine meter in liquid service. A missed filtration spec shifted one diesel line’s K-factor by 0.3% in 14 months. Plan for bearing inspection at every calibration, not only when symptoms appear.
7. How does temperature fluctuation impact the accuracy of the flow measurement?
Temperature changes viscosity and density, and both affect the rotor. A warm fluid is thinner and the K-factor shifts. If you meter at varying temperatures for billing, correct the volume to a reference temperature. Jade Ant lists standard liquid meters from –40 to +200 °C, and the gas and steam model from –20 to +300 °C. Check the bearing and seal limits at your peak temperature.
8. What is the difference between a pulse output and a 4–20 mA output, and can these meters join HART or Modbus networks?
A pulse output is the raw signal, one pulse per blade, best for totalizing and batching. A 4–20 mA output is a scaled current that follows flow rate and works with almost any control system. HART puts digital data on the same 4–20 mA wires, and RS485 Modbus carries more values on one cable. Jade Ant’s gas model lists 4–20 mA, pulse and RS485 Modbus, and its guidance lists HART on smart transmitters. For wireless HART, ask the supplier whether an adapter is supported for your exact model.
9. Are turbine meters suitable for bidirectional flow, or is a check valve required?
Standard models are unidirectional. Jade Ant’s guidance says some models support two-way flow with a dual-channel transmitter. If reverse flow is possible and your meter is one-way, add a check valve to protect the rotor and keep the total clean. Confirm bidirectional ability with the supplier before you rely on it.
10. How often should a municipal utility recalibrate its turbine meters to meet regulatory standards?
Jade Ant’s guidance is every 12 months for municipal water billing, with 6 months for some large revenue meters. Your local regulator has the final word, so check it first. Between calibrations, run in-situ checks against a master meter or tank test, and keep a K-factor log per serial number. That data lets you extend or shorten the interval based on real drift instead of a calendar.