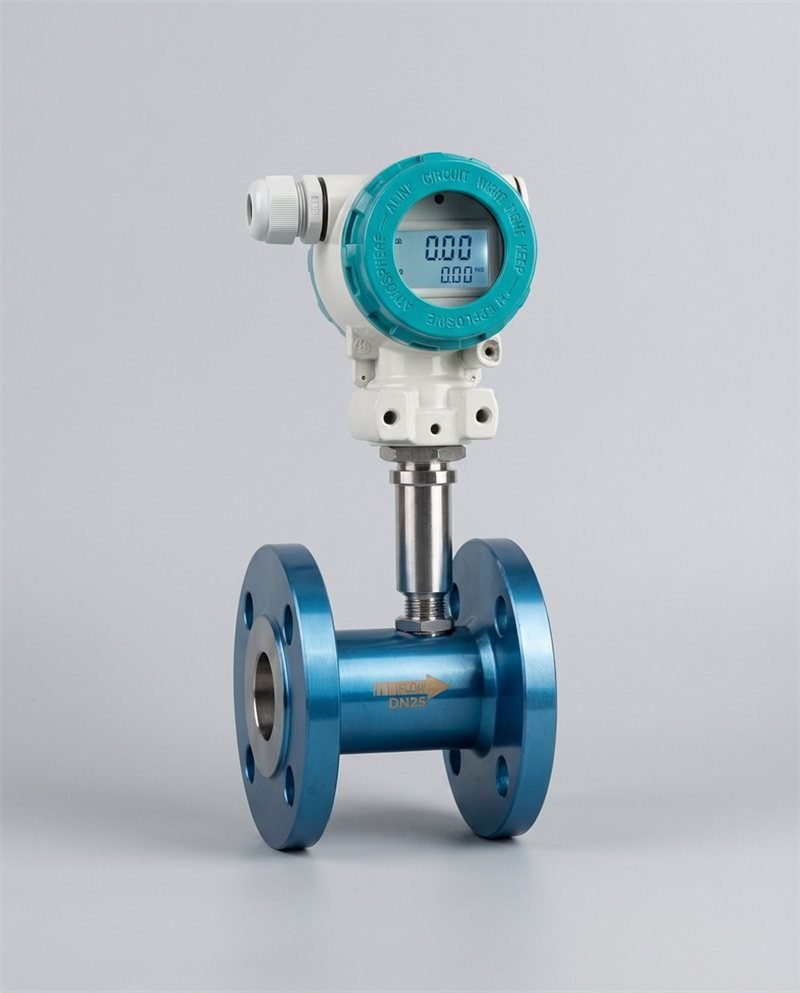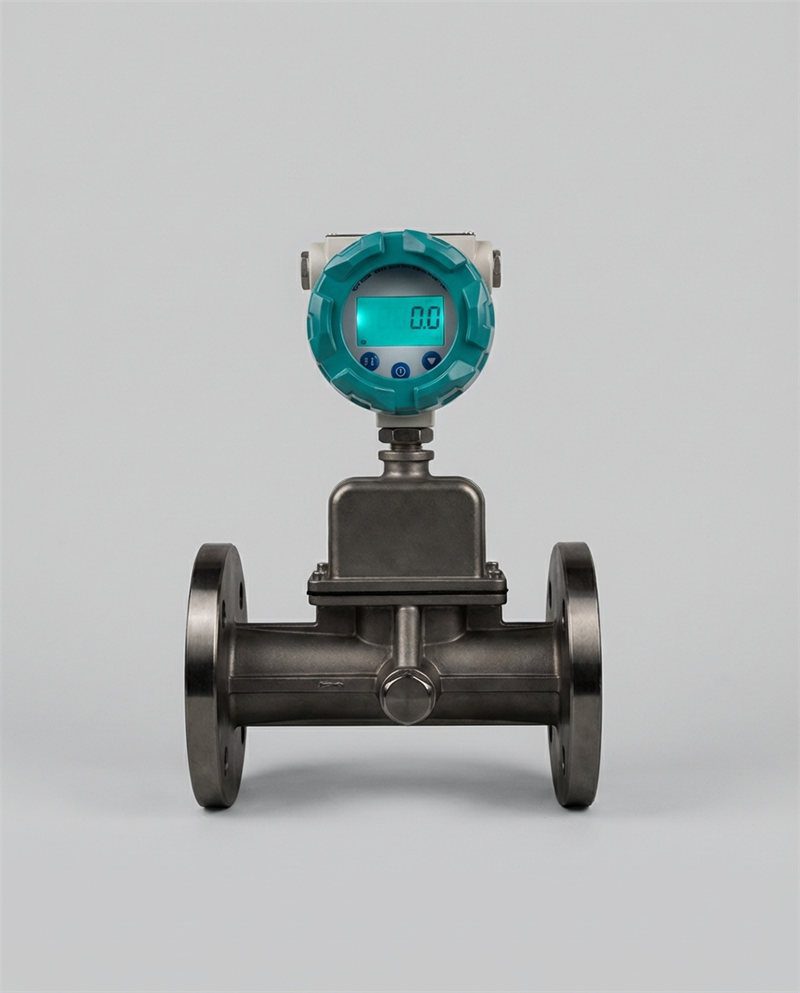
Coriolis vs Ultrasonic Gas Flow Meters: Which Fits Your Plant?
A Strategic Guide for Industrial Decision-Makers
1. Making the Right Flow Meter Choice
Choosing between a Coriolis and an ultrasonic gas flow meter can look like a simple spec-sheet comparison. It usually turns out to be a decision about your whole project: how the skid is designed, what calibration costs over ten years, how audits go, and whether field techs get called out at 2 a.m.
Here is the short version:
- A Coriolis flow meter measures mass flow directly, meaning the actual kilograms or pounds of gas passing through. It does not depend on what the gas is made of. It works best in small to mid-size lines, at high pressure, and wherever precision matters.
- An ultrasonic gas flow meter measures gas velocity using sound waves, then works out volume and standardized flow. It works best in large pipes, clean dry gas, and places where you can’t afford pressure loss or a shutdown.
Why this choice matters. In gas measurement, a 0.5% error sounds small. On a line moving $5 million of natural gas a year, a 0.5% bias works out to $25,000 a year, and it goes unnoticed until someone audits it. Choose the wrong technology and you also pay in pressure drop (compressor energy), extra straight pipe (skid footprint), and recalibration trips.
Who this guide is for:
| Your Role | What You Care About Most | Where to Focus |
|---|---|---|
| OEM / skid-mount manufacturer | Footprint, weight, repeatable accuracy | Sections 4, 5, 10 |
| EPC / system integrator | Design timelines, documentation, protocols | Sections 5, 8, 9 |
| Instrument distributor / importer | Right-first-time quoting, fewer returns | Sections 3, 4, 10 |
| Industrial MRO team | Uptime, recalibration, spare parts | Sections 6, 7 |
| Municipal / utility operator | Large-pipe metering, billing audits | Sections 4, 6, 9 |
Industry insight: Across gas metering tenders we review at Jade Ant Instruments, the single most common specification error is not accuracy. It is choosing a meter by line size instead of by the actual flow range. A 6″ line that runs at 15% of design capacity for most of the year needs a very different meter than one running at 70%.
2. Technology Deep Dive: How Each Meter Works
Coriolis Principle: Mass Flow via Fluid-Induced Tube Vibration
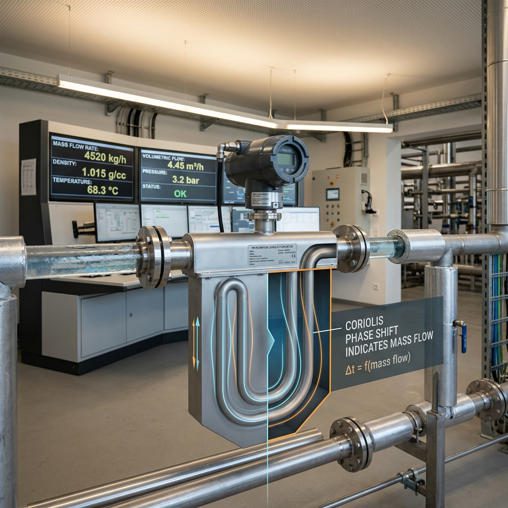
Definition: A Coriolis flow meter sends gas through one or two tubes that are vibrated at their natural frequency. As gas moves through, its mass makes the tubes twist slightly. The meter measures that twist, and the size of the twist is directly proportional to mass flow.
A simple way to picture it: swing a garden hose side to side while water runs through it. The hose bends a little differently because of the moving water. A Coriolis meter measures that bending with electronic sensors, thousands of times per second.
 A Coriolis mass flow meter installed in process piping. Image: Bitjungle via Wikimedia Commons.
El Coriolis effect in flow tubes gives you three readings from one device (background reading):
- Mass flow, from the phase shift (time lag) between the sensors at the inlet and outlet.
- Density, from changes in the tube’s vibration frequency.
- Temperature, from a built-in RTD sensor.
 Animated view: flowing fluid causes the vibrating tube to twist. The twist is what the meter measures. Image via Wikimedia Commons.
Ultrasonic Principle: Time-of-Flight Differential
Definition: A transit-time ultrasonic flow meter sends sound pulses diagonally across the pipe, first with the flow and then against it. A pulse travelling with the gas arrives slightly sooner. The difference in travel time tells you gas velocity. Multiply velocity by the pipe’s cross-section area and you get volumetric flow.
A good comparison is a swimmer crossing a river. Swimming downstream is faster than swimming upstream, and if you time both trips you can work out how fast the river is moving. You can read more about the transit-time principle behind these meters.
 The ultrasonic sound path crosses a fully developed flow profile. Velocity varies across the pipe, which is why multiple paths improve accuracy. Image via Wikimedia Commons.
Watch: Both Principles Explained
This video walks through transit-time ultrasonic measurement in under 10 minutes and is useful for training new field technicians:

Key Differentiators: Direct Mass vs. Inferred Volume
| Característica | Coriolis | Ultrasonic (Transit-Time) |
|---|---|---|
| What it measures | Mass flow (direct) | Velocity → volume (inferred) |
| Needs P & T compensation for standard flow? | No for mass; yes for standard volume only if composition changes | Yes, always |
| Needs gas composition data? | No | Yes, to convert to standard volume or mass |
| Extra outputs | Density, temperature | Speed of sound, signal quality, gain |
| Piezas móviles | Ninguno | Ninguno |
| Obstruction in pipe | Yes (tubes) | None (full bore) |
What This Means for Varying Gas Composition and Pressure
This is where the two technologies really separate.
When your gas composition changes, for example a biogas plant where methane content swings from 55% to 65%, or a blending skid mixing hydrogen into natural gas, an ultrasonic meter’s volume reading may still be correct. However, converting it to mass or energy requires up-to-date composition data from a gas chromatograph. If that data is late or wrong, your mass figure is wrong too.
A Coriolis meter doesn’t need that data. A kilogram of gas is a kilogram whatever it is made of.
Plain-language takeaway: If you bill, blend, or control by mass, and your gas composition moves around, Coriolis removes one whole source of error from the measurement chain.
3. Performance Comparison: Accuracy, Rangeability & Repeatability
Three terms come up throughout this section:
- Accuracy: How close the reading is to the true value.
- Rangeability (turndown): The ratio of the highest to the lowest flow the meter can measure within its stated accuracy. A 100:1 turndown on a 1,000 kg/h meter means accurate readings down to 10 kg/h.
- Repeatability: How closely the meter gives the same reading under the same conditions. This is critical for batch control.
Coriolis: ±0.5% Typical, Up to 100:1 Turndown
- Typical gas accuracy: ±0.5% of reading. Premium models do better.
- Turndown: Up to 100:1. The practical limit for gas is usually set by pressure drop, not by the electronics.
- Composition sensitivity: None for mass flow.
- Repeatability: Typically ±0.25% or better.
Ultrasonic: ±1.0% Typical, 50:1 Rangeability
- Typical accuracy: ±1.0% for general-purpose meters. Multipath, flow-calibrated custody meters can do considerably better.
- Rangeability: Around 50:1.
- Sensitivity: Swirl, a distorted flow profile, and pulsation from nearby compressors or regulators all affect readings.
Typical uncertainty values for general-purpose industrial models. Custody-grade versions of both technologies can perform better.
| Metric | Coriolis | Ultrasónico |
|---|---|---|
| Typical accuracy (gas) | ±0.5% | ±1.0% |
| Turndown | Up to 100:1 | ~50:1 |
| Composition effect | None (mass) | Needs GC data for mass/energy |
| Flow profile sensitivity | Very low | Alta |
| Best line sizes | ½”–6″ (up to ~12″ in some ranges) | 3″–48″+ |
Real-World Impact
Custody transfer. Custody transfer is the point where gas changes ownership and money changes hands. At that point, the uncertainty band becomes a financial risk. Coriolis gives low uncertainty without extra correction steps. Ultrasonic can reach custody-grade performance, but only with multipath design, flow calibration, and strict installation.
Process control. On a burner-management or reactor-feed loop, repeatability matters more than absolute accuracy. Both technologies repeat well, but Coriolis keeps its repeatability even as gas density shifts.
Skid compliance. OEM skid builders often have to pass a factory acceptance test (FAT) with a tight accuracy window. A Coriolis meter’s accuracy doesn’t depend on the piping around it, so a skid that passes FAT in the factory usually passes on site as well. With ultrasonic, site piping that differs from the factory setup can shift results.
For a deeper look at where Coriolis shines and where it struggles, see our full breakdown of Coriolis strengths and trade-offs.
4. Application Suitability: Matching Technology to Use Case
Coriolis Is Ideal For:
High-accuracy gas blending (OEM skids). Examples include hydrogen/natural gas blending, CO₂ dosing, and specialty gas mixing. A blend ratio is a mass ratio, and Coriolis gives mass on both streams directly, with no chromatograph needed in the control loop.
Example scenario: A CNG dispenser builder measuring gas into vehicle tanks at 200–250 bar. Flow starts high and drops to near zero as the tank fills. Coriolis handles both the high pressure and the extreme turndown in a compact ½”–1″ body.
Low-flow, high-pressure applications. Examples are fuel gas to turbines, instrument gas, and injection skids. Small lines under 2″ are where ultrasonic meters struggle and Coriolis is at its best.
Multi-phase tolerance (wet gas scenarios). Coriolis handles light liquid carryover better than ultrasonic, whose sound signal can be scattered or blocked by droplets. Coriolis accuracy still drops with heavy liquid slugs, but the meter keeps reading and its density output flags the problem.
Ultrasonic Is Ideal For:
Large-diameter utility metering (municipal gas distribution). On an 8″, 12″, or 24″ line, a Coriolis meter is heavy, expensive, and often not made in that size for gas at all. A multipath ultrasonic meter is full-bore, meaning nothing blocks the pipe. Its cost also rises slowly with size, so above roughly 6″ it is usually the economic choice.
Clean, dry, steady-flow environments. Pipeline-quality natural gas after filtration and dehydration is the textbook case for ultrasonic.
Non-intrusive retrofits in existing pipelines. Clamp-on ultrasonic transducers mount on the outside of the pipe. There is no cutting, welding, or shutdown. For MRO teams checking an old orifice meter or for sub-metering, this is often the only practical option. Browse more industrial ultrasonic flow meter applications for field examples.
Quick Application Match Table
| Solicitud | Better Fit | ¿Por qué? |
|---|---|---|
| H₂ / NG blending skid | Coriolis | Direct mass ratio, composition-independent |
| CNG dispensing | Coriolis | High pressure, high turndown, small size |
| City gate station (12″+) | Ultrasónico | Large bore, zero pressure drop, bi-directional |
| Biogas with moisture | Coriolis (small line) / Vortex (larger line) | Wet gas tolerance |
| Compressed air sub-metering | Clamp-on ultrasonic or vortex | No shutdown, low cost |
| Fuel gas to boiler/turbine | Coriolis | Mass-based combustion control |
| Flare gas | Ultrasónico | Very wide velocity range, no pressure drop |
Distributor tip: When a customer asks for “a gas meter for a 10-inch line,” ask what the gas is, how dry it is, and what flow it runs at most of the time. That one question separates a Coriolis quote from an ultrasonic quote, and it prevents returns.
5. Installation & Integration: Practical Field Considerations
Coriolis: Supports, Vibration, and Pressure Drop
Straight-run requirements are minimal. Coriolis meters don’t need long straight pipe runs, which is a real advantage on crowded skids. They do need good pipe support upstream and downstream so pipe stress and vibration don’t reach the sensor.
Vibration sensitivity. Coriolis tubes vibrate at a set frequency, typically 80–1,000 Hz depending on design. If a nearby reciprocating compressor or pump puts energy into that band, the zero point can drift. Rigid mounting and physical separation from vibration sources are required.
Pressure drop. Gas has to travel through narrow, often bent tubes, which can cause 0.3–1+ bar of pressure loss at full flow. On a low-pressure line such as landfill gas at 50 mbar, that loss can make Coriolis unusable. Sizing mistakes here are costly. Review these common Coriolis sizing mistakes before you release a data sheet.
Ultrasonic: Low Loss, Bi-Directional, Clamp-On Options
Minimal pressure loss. A full-bore spool piece is essentially an open pipe, so pressure drop is close to zero. That can save real compressor energy.
 An inline ultrasonic measuring spool. The full-bore design means nearly zero pressure loss. Image: Aurloz, CC BY-SA 4.0, via Wikimedia Commons.
Bi-directional measurement. The same meter measures flow in both directions. This is useful in storage, looped networks, and interconnects.
Clamp-on for zero downtime. Transducers strap onto the outside of the pipe. No hot work permit or process shutdown is needed.
 Clamp-on ultrasonic flow meter under laboratory testing. The transducers never touch the gas. Image: Vitalii cfd, CC BY-SA 4.0, via Wikimedia Commons.
The catch: straight pipe. Inline ultrasonic typically needs 10–20 pipe diameters (D) upstream and 5D downstream, or a flow conditioner. On a 12″ line, 20D is about 6 metres (20 feet) of straight pipe. Clamp-on gas measurement also has limits: it works best on metal pipe with gas above modest pressure, since low-pressure gas carries sound poorly. Our clamp-on ultrasonic buyer’s checklist covers those limits in detail.
Implications by Project Type
| Project Type | Coriolis Impact | Ultrasonic Impact |
|---|---|---|
| EPC new build | Short straight runs speed up layout; check ΔP budget early | Reserve straight-run space in the 3D model from day one |
| Retrofit / brownfield | Needs cut-in and shutdown | Clamp-on avoids shutdown entirely |
| Modular OEM skid | Compact, but heavy; add support steel | Long straight runs can increase skid length 30–50% |
6. Maintenance & Lifecycle Costs: TCO Analysis
Total Cost of Ownership (TCO) means everything you spend on a meter over its life: purchase price, installation, calibration, downtime, spare parts, and energy lost to pressure drop.
Coriolis
- No moving parts, so there are no bearings or rotors to wear out.
- Risks: Tube coating from glycol, compressor oil, or sulfur compounds; erosion from particles in the gas.
- Recalibration: Every 2–5 years, depending on how critical the service is. Zero verification can often be done in place.
For intervals, zero checks, and lifespan data, see our Coriolis calibration and lifespan guide.
Ultrasónico
- No contact with the gas (clamp-on) or no obstruction (inline), so wear is very low.
- Risks: Transducer face fouling, cable damage, and flow-profile changes if upstream piping is modified.
- Periodic verification: Speed-of-sound checks against calculated values, plus path-by-path diagnostic reviews.
10-Year TCO Example: 4″ Gas Line (Illustrative)
The figures below are an illustrative model for a 4″ industrial natural gas line. They are not a quote. Actual costs vary by region, supplier, and service.
| Cost Item (USD) | Coriolis | Inline Multipath Ultrasonic |
|---|---|---|
| Meter purchase | 18,000 | 22,000 |
| Installation (piping, supports, labor) | 4,000 | 7,000 |
| Calibration / verification (10 yrs) | 6,000 | 3,500 |
| Downtime cost (10 yrs) | 4,000 | 2,000 |
| Spares & repairs | 2,000 | 1,500 |
| Pressure-drop energy cost (10 yrs) | 5,000 | 500 |
| 10-year TCO | 39,000 | 36,500 |
Where does the money go for a typical Coriolis gas installation over 10 years?
Industry insight: On 4″ lines, the purchase price gap is often smaller than buyers expect. The gap that matters is pressure-drop energy. If your gas is compressed upstream, a Coriolis meter’s pressure loss becomes a real, recurring electricity cost. Below 2″, Coriolis nearly always wins on TCO. Above 6″, ultrasonic almost always does.
7. Environmental & Process Resilience
Temperature, Pressure, and Vibration Tolerance
| Condition | Coriolis | Ultrasónico |
|---|---|---|
| Process temperature | Typically −50 to +200 °C (special models wider) | Typically −40 to +100 °C inline; clamp-on limited by couplant |
| Pressure | Very high (up to 400+ bar in small sizes) | High (ANSI 900–1500 inline); clamp-on needs enough pressure for signal |
| External vibration | Sensitive at tube frequency | Largely immune to mechanical vibration |
| Acoustic noise | Immune | Sensitive: control valves and regulators can drown the signal |
Acoustic noise is a real issue for ultrasonic. A pressure-reducing regulator installed right upstream can produce ultrasonic noise in the same frequency range as the meter. This is one of the most common causes of “meter reads zero” service calls. When you run through gas flow meter troubleshooting steps, check regulator placement first.
Dirty, Wet, or Corrosive Gas
- Wet gas: Coriolis keeps working, and its density reading helps identify liquid carryover. Ultrasonic signals weaken or drop out.
- Dirty gas: Both need filtration. Coriolis tubes can erode, and ultrasonic transducer faces can foul.
- Corrosive gas (H₂S, wet CO₂, chlorine): Coriolis tube material choice is critical, with options such as 316L, Hastelloy, or duplex. Clamp-on ultrasonic avoids wetted parts altogether.
 An industrial mass flow meter. Material and sealing choices set its limits in corrosive gas. Image: Luigi Chiesa, CC BY 3.0, via Wikimedia Commons.
When neither technology suits a wet, dirty, or steam-heavy stream in a larger pipe, a vortex flow meter with built-in T&P compensation is often the practical middle option.
Hazardous (Class I Div 1) and Remote Locations
Class I Division 1 refers to areas where flammable gas may be present during normal operation. Both technologies are available with explosion-proof or intrinsically safe certifications (FM, CSA, ATEX, IECEx). Always check the full marking against your site’s hazardous area classification.
Para remote, solar-powered sites such as wellheads or rural regulator stations, power draw matters. Many ultrasonic meters run at a few watts. Coriolis transmitters typically need more power, which can mean a larger solar panel and battery bank.
8. Digital Integration & Industry 4.0 Readiness
Communication Protocols
Both technologies commonly support:
- 4–20 mA with HART: An analog signal with digital data layered on top. It is the default in most plants.
- Modbus RTU/TCP: A simple, widely used digital protocol, popular with PLCs and flow computers. See the Modbus protocol specifications.
- Foundation Fieldbus / PROFIBUS: Fully digital networks used in larger DCS systems. HART and Foundation Fieldbus are both managed by the FieldComm Group.
- Pulse/frequency outputs: For totalizers and flow computers.
Diagnostics: What Each Meter Tells You
| Diagnostic | Coriolis | Ultrasónico |
|---|---|---|
| Primary health check | Tube frequency, drive gain, zero stability | Signal strength, gain, SNR per path |
| Process insight | Density, temperature (detects composition shift, liquids) | Speed of sound (compare to GC-calculated value) |
| Fault detection | Coating, erosion, gas entrainment | Path failure, fouling, profile distortion |
| In-situ verification | Built-in meter verification (many models) | Path comparison, speed-of-sound check |
Value for System Integrators
Speed of sound (SoS) is one of the most useful and least used diagnostics in gas measurement. The ultrasonic meter measures SoS itself, and your gas chromatograph data lets you calculate what SoS should be. If the two differ by more than about 0.2%, something is wrong: a fouled path, an incorrect GC reading, or a temperature sensor fault.
On the Coriolis side, a density trend that drifts slowly over months often points to tube coating, which you can catch before accuracy suffers.
Integrator tip: When building a SCADA or IIoT dashboard, don’t stop at flow rate. Bring in drive gain (Coriolis) or per-path gain and SoS deviation (ultrasonic). These are the early-warning signals that make predictive maintenance work.
9. Regulatory & Custody Transfer Compliance
Key Standards at a Glance
| Estándar | Covers | Issued By |
|---|---|---|
| AGA Report No. 11 / API MPMS Ch. 14.9 | Natural gas measurement by Coriolis meters | American Gas Association / API |
| AGA Report No. 9 | Natural gas measurement by multipath ultrasonic meters | American Gas Association |
| OIML R 137 | Gas meters for legal metrology | OIML |
| API MPMS | Petroleum measurement practices | American Petroleum Institute |
Coriolis: AGA #11 for Gas Custody Transfer
AGA 11 sets performance, installation, and calibration practice for Coriolis gas meters. Its second edition tightened the performance requirement for gas meters. See this AGA Report No. 11 performance update for context. A key finding in the industry is that water-calibrated Coriolis meters can be used on gas with documented uncertainty. That saves money, because gas calibration facilities are expensive and often booked out.
Ultrasonic: AGA #9 with Strict Installation Guidelines
AGA 9 is a performance-based specification. It sets maximum error limits, repeatability, and resolution, and requires flow calibration for custody use. It also puts heavy weight on installation effects. This overview of AGA Report No. 9 explains how the standard evolved.
In practice, an AGA 9 meter is only as compliant as its upstream piping. If the site changes that piping after calibration, the calibration may no longer be valid.
Audit Readiness Checklist
For utility billing and EPC handover packages, have these ready:
- Calibration certificates with traceability to national standards.
- As-found / as-left records from every recalibration.
- Installation drawings showing straight runs and conditioners (ultrasonic).
- Zero verification logs (Coriolis).
- Diagnostic snapshots at commissioning, used as your “fingerprint” baseline.
- Gas composition source and update frequency (for ultrasonic energy calculations).
For a side-by-side on how calibration differs across technologies, read how calibration differs across thermal, Coriolis, and vortex meters.
10. Decision Framework: 10 Critical Questions to Ask Before Choosing
Use this as a pre-quote checklist. Each answer points toward one technology.
| # | Question | Points Toward Coriolis If… | Points Toward Ultrasonic If… |
|---|---|---|---|
| 1 | Is the gas composition variable or unstable? | Yes: biogas, blends, H₂ mixes | No: pipeline-quality, stable |
| 2 | Do you require true mass flow without external compensation? | Yes | Volume or standard volume is fine |
| 3 | What are your turndown and low-flow accuracy requirements? | >50:1, or accurate at very low flow | ≤50:1, steady flow |
| 4 | Is the installation in a high-vibration or constrained space? | Constrained space, low vibration | High mechanical vibration, room for straight runs |
| 5 | Are you supporting custody transfer or internal allocation? | Custody transfer, small/mid lines | Custody transfer on large lines (AGA 9), or allocation |
| 6 | What is the expected gas cleanliness and moisture content? | Some moisture or liquid carryover | Clean, dry, filtered |
| 7 | Do you need non-invasive installation or hot-tap capability? | No, a cut-in is acceptable | Yes: clamp-on or hot-tap insertion |
| 8 | What are your long-term maintenance and recalibration resources? | Access to calibration lab every 2–5 yrs | Prefer in-situ verification |
| 9 | Are you integrating with a central SCADA or IIoT platform? | Want density + rich health data | Want SoS + path diagnostics |
| 10 | What is your total project budget—capex vs. opex priorities? | Small line, low ΔP penalty | Large line, energy costs matter |
How to score it: If 7 or more answers point one way, you have your answer. If it is close to 5–5, the deciding factor is usually line size (under 4″ favors Coriolis, over 6″ favors ultrasonic) or gas quality.
Still undecided? You can compare the leading mass flow meter brands to see how specs differ between suppliers. Or send your process data sheet with gas type, pressure, temperature, and flow range. The Jade Ant Instruments application team will send back a sizing recommendation with the calculations, typically within 24 hours.
Glossary: Key Terms in Plain Language
| Term | Simple Definition | Example |
|---|---|---|
| Mass flow | Weight of gas passing per unit time | 250 kg/h of natural gas |
| Volumetric flow | Space the gas occupies per unit time, at line conditions | 40 m³/h at 10 bar |
| Standard volume | Volume corrected to reference conditions (e.g., 15 °C, 1.01325 bar) | 400 Sm³/h |
| Turndown | Max-to-min measurable flow ratio | 100:1 means 1,000 → 10 kg/h |
| Transferencia de custodia | Measurement where gas changes ownership and gets billed | City gate station |
| Straight run (D) | Straight pipe length in multiples of pipe diameter | 10D on 6″ pipe ≈ 1.5 m |
| Flow conditioner | A plate or tube bundle that removes swirl and evens out the flow profile | Perforated plate 10D upstream |
| Speed of sound (SoS) | How fast sound travels in the gas; depends on composition, pressure, temperature | ~430 m/s in methane at ambient |
| Zero stability | The reading a Coriolis meter drifts to at zero flow | ±0.5 kg/h |
| Drive gain | Energy needed to keep Coriolis tubes vibrating; a rise can mean gas bubbles, liquid, or coating | Jump from 5% to 40% |
| Pressure drop (ΔP) | Pressure lost across the meter | 0.5 bar at full flow |
| Multipath | Ultrasonic meter with several sound paths for better accuracy | 4-path or 8-path chordal meter |
Frequently Asked Questions (FAQs) – From Industry Professionals Like You
1. Can ultrasonic meters measure mass flow directly like Coriolis? No. Ultrasonic meters infer mass flow using pressure and temperature compensation plus gas composition data. Coriolis measures mass directly.
2. Which meter is better for natural gas custody transfer? Coriolis is preferred for high-accuracy, variable-composition custody transfer, especially in smaller lines. Ultrasonic is viable, and dominant on large lines, when it is AGA 9 compliant, flow-calibrated, and well maintained.
3. Do Coriolis meters work well with wet or dirty gas? Yes. Coriolis handles wet gas better than ultrasonic, though heavy slugging or coating can affect performance. Its density reading also helps you detect liquid carryover.
4. Are ultrasonic meters suitable for small pipe sizes (<2″)? Typically not. Ultrasonic meters are most effective in 3″ and larger lines, while Coriolis excels in smaller lines.
5. What is the typical lifespan of each meter type? Both last 10–15+ years with proper maintenance. Coriolis may need earlier recalibration in harsh, erosive, or coating conditions.
6. Can I retrofit an ultrasonic meter without cutting the pipe? Yes. Clamp-on ultrasonic meters install without touching the process, which makes them a good fit for MRO and utility upgrades. Confirm that gas pressure and pipe material support a strong enough signal.
7. How do ambient vibrations affect Coriolis meters? High vibration near the tube’s resonant frequency can disturb readings and zero stability. Proper mounting, pipe supports, and distance from compressors are critical.
8. Do ultrasonic meters require straight pipe runs? Yes. Typically 10–20D upstream and 5D downstream, or a flow conditioner. The goal is a fully developed, symmetrical flow profile without swirl. (Gas flow in industrial pipes is almost always turbulent, so the aim is a stable profile, not laminar flow.)
9. Which meter offers better turndown for variable flow processes? Coriolis typically offers better turndown (up to 100:1), which makes it ideal for batch and load-following systems.
10. Is density measurement possible with ultrasonic meters? Not directly. Coriolis gives real-time density, which is valuable for gas quality monitoring and blending. Ultrasonic gives speed of sound, which is useful as a diagnostic but is not density.
11. How often should each meter be calibrated? Coriolis: every 2–5 years. Ultrasonic: verification every 3–6 years, depending on how critical the application is and what your regulator requires.
12. Which technology integrates more easily with PLC/SCADA systems? Both support standard protocols such as HART, Modbus, and Foundation Fieldbus. Coriolis offers richer process diagnostics (density, drive gain) for predictive maintenance.
13. Are there size and weight limitations for Coriolis in skid designs? Yes. Coriolis meters are heavier but more compact in length, so OEM skids need structural support. Above about 6″, weight and cost rise sharply for gas service.
14. Can ultrasonic meters detect flow reversals? Yes. Bi-directional measurement is a standard feature, useful in utility loop systems, storage, and interconnects.
15. What training is required for field technicians to maintain these meters? Coriolis: basic calibration tools, zero-verification procedures, and safety practices. Ultrasonic: signal interpretation, speed-of-sound checks, and path alignment checks.
Designed for engineers, procurement leads, and technical decision-makers in OEM, EPC, distribution, and utility operations. This guide cuts through marketing claims to give practical guidance for choosing the right flow meter.